



Design da Profundidade do Copo de Punção para Tablet: Formato, Força, e Risco de Defeitos
Tablet punch cup depth helps determine the finished tablet’s face curvature, central band, and overall appearance. A deeper cup can create a more convex tablet, but it may also reduce punch-tip strength and increase sensitivity to capping, uneven density, or wear under certain operating conditions.
There is no universal best cup depth. The correct design depends on cup radius, Diâmetro do tablet, land geometry, required compression load, Comportamento de formulação, e condições de imprensa. Cup depth should therefore be evaluated as one part of the wider system of Tipos de ferramentas para press de tablets, not as an isolated dimension.
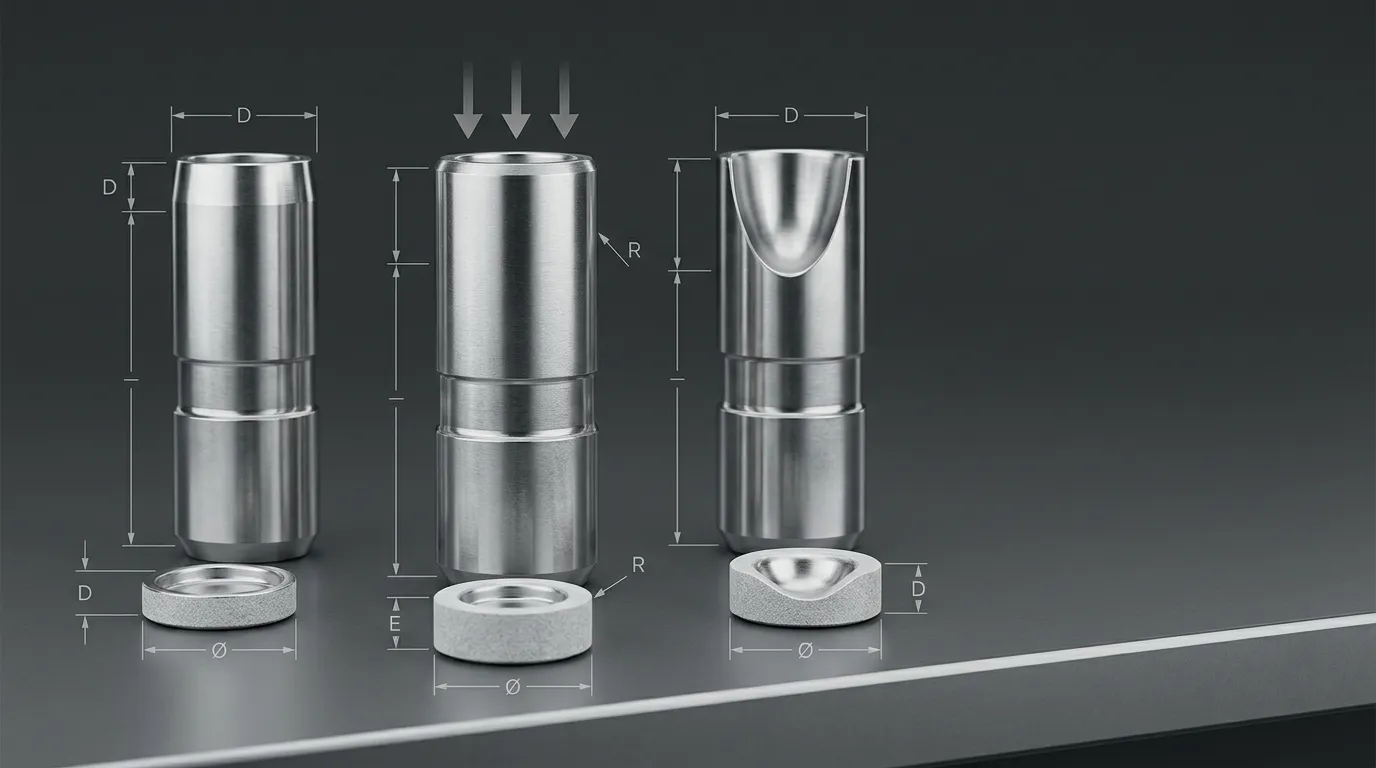
O que a profundidade do copo perfurador para tablet mede
The punch cup is the recessed area at the end of the punch tip. During compression, the upper and lower cups form the two main faces of the tablet while the die bore forms its central band or sidewall.
Cup depth is the vertical distance from the highest reference surface of the punch tip to the lowest point of the cup. Identification features such as embossed or debossed letters should not be included in this measurement. This distinction follows the terminology used in the Manual de Especificação de Tableting APhA.
Cup depth is also separate from punch working length. Working length influences compression position and tablet consistency, while cup depth defines the shape of the tablet face.
Cup Depth, Cup Radius, and Cup Volume Are Different Variables
Cup depth alone does not fully describe the punch profile.
| Variável | O que ela descreve | Por que isso importa |
|---|---|---|
| Profundidade do copo | A distância vertical da superfície de referência até o ponto mais baixo do copo | Influences face height, tablet convexity, and remaining punch-tip section |
| Raio da taça | A curvatura usada para formar a taça | Determina quão gradual ou acentuadamente a face curva |
| Volume da copa | O volume contido dentro do perfil recuado | Afeta como o volume do tablet é distribuído entre as faces e a faixa central |
| Relação R/D | Raio do copo dividido pelo diâmetro do comprimido | Ajuda a comparar a curvatura entre tablets de diferentes tamanhos |
Two punches can have similar cup depths but different radii. One may use a smooth, broad curve, while another reaches the same depth through a steeper profile. Their tablet appearance, stress distribution, and punch-tip strength may therefore differ.
Compound cups make this distinction even more important. Instead of using one continuous radius, a compound profile combines two or more radii. This can create a smooth-looking tablet face while still producing a steep transition near the outer edge.
Como as taças superior e inferior formam a banda do comprimido e a espessura total
The finished tablet consists of three connected geometric regions:
- the upper cup-formed face;
- the lower cup-formed face;
- the central band formed inside the die.
For a given total tablet thickness, increasing the combined depth of the upper and lower faces generally leaves less thickness in the central band. A narrower band changes the tablet’s proportions and may influence die-wall contact, Comportamento de ejeção, and mechanical failure patterns.
Tablet diameter must also be considered. A 1 mm cup depth does not represent the same curvature on a small tablet and a large tablet. Diâmetro, Raio, Profundidade, and band thickness must be reviewed together.
Upper and lower cup profiles do not always have to match. A tablet may use symmetrical faces, or one side may be flatter to support branding, Manejo, Revestimento, Embalagem, ou requisitos de inscrição. Any asymmetrical design should still be evaluated as one complete tablet geometry.
Como os Perfis Comuns de Copos de Ponche se Comparam
The names used for cup profiles describe general forms rather than one universal set of dimensions. A “deep concave” profile from one tooling system or supplier may not have exactly the same depth or radius as another.
| Perfil da taça | Forma geral | Principal benefício de projeto | Principal limitação ou risco |
| Face plana | Superfície plana de tábua | Geometria simples e carga relativamente direta | Pode não fornecer a aparência ou as características de manuseio necessárias |
| Flat-faced bevel edge, or FFBE | Centro plano com aresta inclinada | Define a borda do tablet e pode reduzir um canto mais agudo | A geometria do bisel afeta a seção externa da ponta e a borda do tablet |
| Flat-faced radius edge, or FFRE | Centro plano com aresta arredondada | Proporciona uma transição de borda mais suave | Detalhes do raio ainda afetam o estresse e o comportamento compacto |
| Côncavo raso | Face de comprimido ligeiramente convexo | Proporciona curvatura enquanto preserva uma faixa central relativamente substancial | Pode não atender a um requisito de aparência fortemente convexa |
| Côncavo padrão | Curvatura moderada da face | Equilibra aparência e praticidade geral das ferramentas | "Padrão" não representa uma dimensão universal |
| Côncavo profundo | Face fortemente convexa | Cria um perfil de tablet mais pronunciado | Pode reduzir a capacidade de força da ponta do punção e aumentar a sensibilidade ao caping |
| Côncavo extra-profundo | Face altamente convexa | Suporta uma forma característica de tablete arredondada | Produz uma geometria mais agressiva e requer força cuidadosa e revisão da formulação |
| Copo composto | Face criada a partir de múltiplos raios | Permite mais controle sobre aparência e formato das bordas | A profundidade sozinha não pode descrever suas implicações de tensão ou resistência |
A profile should not be selected solely from this classification. The actual drawing must specify the relevant depth, radius or radii, Terra, edge transition, Diâmetro do tablet, and total thickness.
Por que a geometria do copo mais profunda pode reduzir a capacidade da força do soco
The tablet press may be capable of applying a high compression force, but that does not mean every punch-tip design can safely carry that load.
A deeper or steeper cup removes more material from the punch-tip region and changes the path through which compression load passes. The allowable force can depend on:
- tip diameter and shape;
- cup depth and radius;
- single-radius or compound geometry;
- land width and transition geometry;
- punch material and heat treatment;
- existing wear or damage;
- the safety margin applied by the tooling designer.
Specialist tooling guidance consistently warns that machine capacity and punch-tip capacity are separate limits. A tooling design should therefore receive a drawing-specific force assessment rather than relying only on a generic press rating or tooling class.
A SunshinePro lista o Premium High-Speed Steel para seus Ferramentas para prensa de tablets. Material is one contributor to strength, but it does not replace a geometry-specific review of the punch tip.
Como as transições entre terra e copo e borda afetam a resistência da ponta
The land is the narrow flat area around the perimeter of the punch tip. It provides support at the edge of the cup and influences wear, Flashing, and tablet-band appearance.
A wider or better-supported land may improve edge strength, but changing it can also alter the tablet profile. The transition between the cup and land matters as well. A smooth blend radius generally creates a less abrupt geometric change than a sharp corner.
These details cannot be selected independently:
- Cup depth affects how much material remains beneath the recessed face.
- Land width affects edge support.
- The blend radius affects the transition between the cup and land.
- Tablet appearance limits how much these features can be changed.
There is no universal minimum land width. The correct value depends on the punch shape, Material, compression requirement, tablet appearance, e padrão de ferramentas.
Compression Force, Pressão, Breaking Force, and Tensile Strength
Several different measurements are used in tablet design, and they should not be treated as synonyms.
| Mandato | Significado |
| Força de compressão | The load applied by the tablet press, commonly expressed in kilonewtons |
| Pressão de compressão | Force divided by an applicable area, commonly expressed in megapascals |
| Força de quebra de tablets | A força medida necessária para quebrar uma tábua finalizada em um teste definido |
| Resistência à tração | Uma medida ajustada pela geometria usada para comparar a resistência mecânica de tablets |
Compression pressure is often used in research because the same force produces different pressure conditions on tablets with different face areas.
Breaking force is a direct test result. Tensile strength attempts to account for tablet dimensions and geometry, making it more useful for some comparisons. Highly convex or unusual profiles may require an equation appropriate to that geometry rather than a formula developed for a flat cylindrical tablet.
Como a Profundidade do Copo Influencia a Mecânica dos Tablets e o Risco de Defeitos
During compression, powder does not densify uniformly in every region of a tablet. Punch shape affects how material moves, how pressure is transmitted, and where density or stress gradients develop.
Finite-element and experimental studies have found that convex punch profiles can produce more heterogeneous density distributions than flat punches. Reduced curvature radius and changes in tablet thickness may increase those gradients under the conditions studied. The effect is important because regions with different density or residual stress may respond differently during decompression and ejection.
These findings are directional, not universal. The actual result also depends on formulation properties, compression pressure, Velocidade, Lubrificação, Liberação ao ar, Diâmetro do tablet, and band thickness.
Por que o risco de limitamento não pode ser previsto apenas pela profundidade
Capping occurs when part of the upper or lower crown separates from the tablet body. Research published in Pesquisa Farmacêutica found that increasing punch cup depth was associated with a higher capping index in the studied acetaminophen formulation and compression conditions.
Um estudo separado na Revista Internacional de Farmacêutica showed that tablet diameter, band thickness, curvature ratio, and their interactions influenced capping behavior. Greater curvature, a thinner band, and larger diameter increased capping susceptibility in that experimental system.
These studies do not prove that every deep cup will cap. They show that geometry can increase risk when combined with particular material and process conditions.
Cup-depth assessment should therefore include:
- Diâmetro do tablet;
- upper and lower curvature;
- central band thickness;
- formulation compactibility;
- Recuperação elástica;
- target compression pressure;
- press speed and air-release conditions;
- existing capping history.
A shallower cup may reduce one geometric risk while failing to meet appearance, Revestimento, Manejo, or dosage-form requirements. The design decision is a trade-off, not a simple ranking.
Distinguishing Capping, Laminação, Air Entrapment, and Tool Wear
Not every separation defect is caused by the cup profile.
| Observação | Possível causa relacionada à geometria | Outra possível causa | O que verificar |
| A coroa se separa da tábua | Aggressive curvature, thin band, Concentração de tensão | Recuperação elástica, entrapped air, unsuitable pressure or speed | Local da falha, Perfil da copa, Resposta de formulação, Condições de imprensa |
| Tablet se separa por meio de um plano interno | Distribuição desigual de densidade ou tensões | Lubrificação, formulation weakness, air pressure | Fracture plane, density pattern, material and process history |
| Um material fino aparece ao redor da faixa do tablet | Damaged or worn land, clearance issue | Die wear, Alinhamento, força excessiva | Punch edge, land condition, O Furo, Alinhamento |
| Os defeitos aumentam após o uso prolongado da ferramenta | A geometria efetiva do copo ou do terreno mudou | Deriva do processo ou variação da formulação | Compare ferramentas desgastadas com registros originais de inspeção |
| Danos locais aparecem próximos à borda da tábua | J-hooking ou borda de punção danificada | Problema de manuseio ou ejeção | Inspeção e comportamento de ejeção da ponta ampliada |
Entrapped air is one important non-geometric factor. Research in the Journal of Pharmaceutical Sciences shows that internal air pressure can rise during compression and contribute to cracking or capping. Powder permeability, compression speed, tablet size, and consolidation behavior all affect this mechanism.
Como Selecionar a Profundidade do Copo para um Tablet Novo ou Revisado
A useful selection process begins with the required tablet, not with a preferred punch profile.
- Define the finished tablet shape and dimensional limits.
- Select depth and radius together.
- Review the remaining band and edge geometry.
- Estimate the required production compression conditions.
- Confirm the allowable force for the proposed punch tip.
- Review formulation and process sensitivity.
- Compare less aggressive alternatives.
- Validate the final design through compression trials and inspection.
Comece com o formato e a faixa do tablet exigidos
Document the dimensions and functional requirements before choosing the cup profile:
- tablet diameter or major and minor axes;
- target total thickness;
- required band thickness;
- upper and lower face shape;
- edge style;
- coating and handling requirements;
- branding or identification area;
- packaging and feeding constraints.
The design team should then determine whether the appearance can be produced with a broader radius or shallower depth. A small geometric change may preserve the visual profile while increasing punch-force margin or reducing capping sensitivity.
Upper and lower profiles should also be assessed separately. A symmetrical tablet may be visually desirable, while an asymmetrical tablet may provide a flatter identification surface or better handling characteristics.
Verifique a Formulação e a Sensibilidade ao Processo
The same cup geometry can behave differently with two formulations. Relevant material properties include:
- compactibility;
- plastic or brittle deformation behavior;
- Recuperação elástica;
- permeability;
- lubricant sensitivity;
- condição de umidade;
- previous capping or lamination history.
Press conditions matter as well. Precompression may assist air release and early consolidation, while press speed affects the time available for densification and decompression. Detailed consolidation-time decisions belong to Cabeça de perfuração para tablet plana e tempo de permanência, but cup depth should still be reviewed alongside those conditions.
Geometry cannot automatically compensate for a formulation that does not form a stable compact. It also should not be changed before confirming that the defect is not being caused by air entrapment, Lubrificação, Pressão, Velocidade, Alinhamento, or worn tooling.
Confirme a margem de força da ferramenta e valide o projeto final
Before manufacturing the full tooling set, confirmar:
- the press and tooling standard;
- the proposed upper and lower cup drawings;
- the material and heat-treatment specification;
- the expected operating-force range;
- the allowable punch-tip force for the proposed geometry;
- the required safety margin;
- the cup, Terra, Raio, and working-length tolerances;
- the trial and acceptance criteria.
Production trials should use the actual formulation, intended press, realistic operating speed, and expected pressure range. Evaluation should include tablet dimensions, Aparência, breaking behavior, Finalização, Laminação, Ejeção, e condição de punção.
A profile is ready for approval only when both sides of the design are acceptable: the punch can withstand the operating conditions, and the formulation can produce a stable tablet with the required shape.
O que especificar no desenho do perfurador e na RFQ
A tooling supplier cannot assess cup depth from a tablet image alone. The RFQ should separate the required tablet geometry from the tooling, Imprensa, e condições de produção.
SunshinePro states that custom tablet tooling can be processed from drawings or samples and that its workflow includes drawing submission, Revisão de design, citação, Produção, Inspeção, and delivery. A controlled drawing remains the clearest way to define the required geometry.
Geometria e Informações de Aplicação incluem
| Informações | Por que isso importa |
| Diâmetro do tablet ou eixos maior e menor | Estabelece a escala da geometria da face |
| Espessura total do alvo | Define o perfil completo acabado |
| Espessura da faixa necessária | Controla a parede lateral central e a região de contato do chip |
| Profundidades das taças superior e inferior | Define cada face de forma independente |
| Raio de copa ou raios compostos | Descreve a curvatura, e não apenas a profundidade |
| Largura do terreno | Define suporte a borda perfurada e borda de tablets |
| Raio de mistura ou transição | Controla a transição da taça para a terra |
| Estilo de borda | Afeta a borda da mesa e a geometria do perfurador |
| Relevo ou relevo | Altera a geometria local e as características de identificação |
| Padrão de prensa e ferramentas para tablets | Confirma compatibilidade física |
| Faixa esperada de força ou pressão | Suporta revisão da resistência das ferramentas |
| Formulação e histórico conhecido de defeitos | Identifica riscos específicos da aplicação |
| Requisitos de superfície e inspeção | Estabelece critérios de aceitação |
A supplier should also know whether an existing tablet or punch sample is being reproduced. A sample may help communicate shape, but it should not replace a controlled drawing when exact depth, Raio, Terra, and tolerance matter.
Tolerância, Inspeção, and Documentation Requirements
Feature-specific tolerances should be agreed on the drawing. A general supplier capability does not prove that every cup feature can or should use the same tolerance.
Define how the following will be checked:
- upper and lower cup depth;
- cup radius or profile;
- Largura do terreno;
- tip dimensions;
- Comprimento de trabalho;
- Comprimento total;
- consistency across the punch set;
- material identification;
- final inspection records.
SunshinePro’s tablet tooling page publishes a general tolerance capability of ±0.002 mm and states that material inspection reports can be provided. That figure should still be confirmed against the actual cup feature, drawing geometry, Método de inspeção, and production requirement.
É declarado Abordagem de controle de qualidade includes raw-material inspection, Monitoramento em processo, Testes finais, e relatórios de inspeção. Buyers should specify which records are required for the particular tooling order.
Como o desgaste pode alterar a profundidade efetiva do copo e o risco de defeitos
An approved cup design can change during production life.
Repeated polishing may gradually reduce effective cup depth, alter the radius, narrow the land, or round the edge transition. Uneven wear across a punch set can also produce differences in tablet thickness or face shape.
Common wear-related warning signs include:
| Sintoma de produção | Verificação de ferramentas |
| A face do tablet fica menos definida | Compare a profundidade e o perfil do copo com o desenho aprovado |
| Mudanças na aparência da banda tablet | Inspect land width, edge transition, e condição de morte |
| A cobertura aparece após um período de produção estável | Check for J-hooking, worn land, Geometria do copo alterada, and process drift |
| As dimensões variam conforme a estação | Compare os socos em todo o conjunto |
| Aparecem flashes ao redor da faixa | Inspect punch-tip edges, A Liberação, Desgaste, e alinhamento |
J-hooking occurs when the punch-tip edge becomes deformed or develops a hooked profile. This damaged edge may disturb tablet release and contribute to capping, Laminação, or flashing.
Before redesigning the cup, compare the current tooling with its original measurement and inspection records. A design that performed correctly when new may be experiencing a maintenance or wear problem rather than a fundamental geometry error.
Erros comuns de design na profundidade do copo
- Selecionar a profundidade apenas pela aparência do tablet
Appearance does not reveal punch-tip strength, density distribution, or formulation sensitivity. - Tratando profundidade e raio como intercambiáveis
Two profiles with the same depth can have different curvature and stress behavior. - Ignorando o diâmetro do tablet
A fixed depth has a different meaning on different tablet sizes. - Ignorando a banda central
Deeper faces may reduce band thickness and change mechanical behavior. - Uso da capacidade da máquina como limite de força de punção
The press may be able to apply more load than the punch tip can safely withstand. - Deixando detalhes sobre terra e transição indefinidos
The cup edge is part of the structural design, not a minor finishing feature. - Assumindo que todas as tapas profundas causam tampas
Depth may increase susceptibility, but formulation and process conditions determine the actual result. - Assumindo que copos rasos eliminam defeitos
Capping and lamination can still result from air, Recuperação elástica, Lubrificação, Pressão, Desgaste, or other causes. - Copiar um perfil de outro diâmetro de tablet
The depth-to-diameter and radius-to-diameter relationships may be different. - Ignorando o desgaste das ferramentas
A worn punch may no longer match the approved cup profile. - Aplicando uma tolerância geral a cada característica
Profundidade do copo, Raio, Terra, and working length may require different controls. - Aprovação do desenho sem testes relevantes para produção
Dimensional correctness does not prove formulation compatibility.
Quando Envolver um Fornecedor de Ferramentas para Tablets
Supplier review is useful when the cup is deep, compound, asymmetrical, unusually small, intended for high compression load, or associated with recurring tablet defects. It is also appropriate when an existing punch or tablet sample must be reproduced.
SunshinePro's Ferramentas para prensa de tablets page confirms punches and dies, Aço Premium de Alta Velocidade, standard and non-standard size options, and customization based on drawings or samples. It also states that material inspection reports are available.
Antes de fazer um pedido, request drawing-specific confirmation of:
- upper and lower cup geometry;
- Material;
- feature tolerances;
- press and tooling compatibility;
- Método de inspeção;
- Documentação;
- allowable punch-tip force.
SunshinePro does not publicly confirm formulation testing, finite-element analysis, capping trials, or pharmaceutical-process validation. Those requirements should be discussed and verified separately rather than assumed from its general tooling capabilities.
Once the tablet geometry, expected operating conditions, and inspection requirements are defined, envie o desenho ou amostra das ferramentas for manufacturing review and quotation.
Compartilhe:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
