



Pinos de núcleo para moldes de injeção: Projeto, Material, e Guia de Tolerância
Core pins are precision mold components used to form internal holes, recesses, and posts inside plastic parts. Choosing the right material, Tolerância, Acabamento superficial, and cooling design affects molded part accuracy, Vida útil do molde, e custo de manutenção. Pinos padrão funcionam para muitos moldes, but custom core pins are often required for thin walls, Resinas abrasivas, deep features, e aplicações de tolerância apertada.
Precision internal features can make or break a molded part. A poorly designed core pin may cause flash, Deriva dimensional, cooling issues, or early mold failure. Buyers and mold engineers need more than a catalog diameter. They need the right material, Geometria, finish, and support strategy for the application. This guide explains how to choose and specify core pins that hold tolerances and survive production cycles.
What are core pins in injection molds?
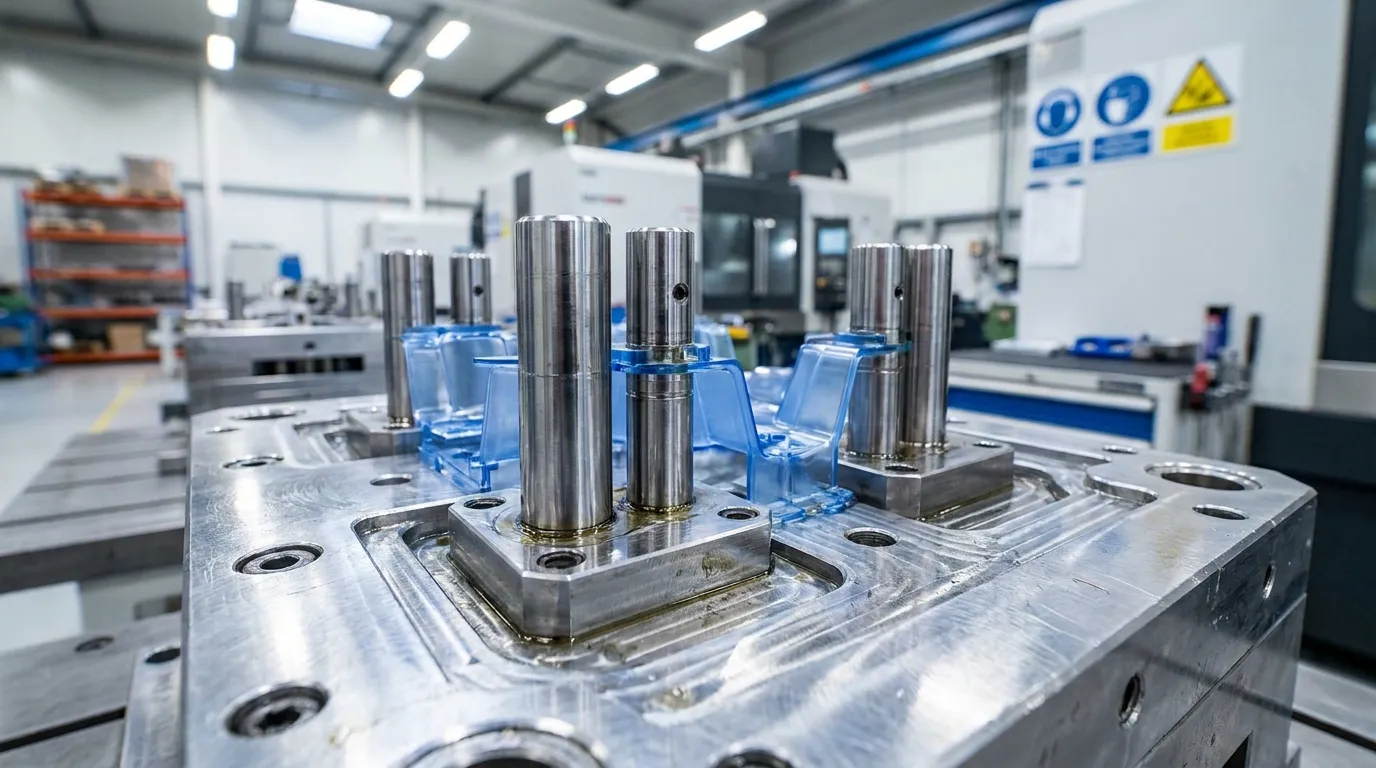
Core pins are precision mold components used to create internal holes, recesses, or posts in molded parts. Manufacturers often use separate core pins instead of machining mold steel directly because pins are easier to replace, maintain, and manufacture with tight tolerances.
In injection molding, a core pin extends into the mold cavity to shape internal geometry. When molten plastic flows around the pin and cools, it leaves behind a hole or internal feature. Core pins are common in medical connectors, Clipes automotivos, Caixas eletrônicas, and threaded plastic parts.
Most molds use removable core pins instead of machining every detail directly into the cavity block. This approach simplifies maintenance and allows damaged or worn pins to be replaced without rebuilding the entire mold. Suppliers such as DME categorize core pins as standard mold components because they are widely used across injection molding systems.
| Função do pino central | Exemplo típico |
|---|---|
| Criação de buracos internos | Furo do parafuso da carcaça de plástico |
| Pino interno fino | Recurso do conector eletrônico |
| Cavidade cilíndrica profunda | Instalação de tubos médicos |
| Característica de alinhamento | Componente plástico de encaixe rápido |
For a broader overview of mold systems and related components, Veja isso Guia de componentes de molde.
Why use separate core pins instead of machining the mold directly?
Separate core pins simplify maintenance and improve manufacturability. Thin or deep internal features are often too fragile to machine directly into mold steel, so replaceable pins reduce repair cost and downtime when wear or breakage occurs.
Small internal geometries can be difficult to machine directly into a cavity block. A removable pin gives mold makers more flexibility during grinding, Polimento, and heat treatment. If the feature wears out, technicians replace the pin instead of repairing the full mold insert.
This matters most in high-cycle production. A mold producing automotive clips or consumer electronics may run hundreds of thousands of cycles per year. Replacing a damaged pin is faster and cheaper than machining a new cavity section.
| If the Mold Needs... | Separate Core Pins Help Because... |
|---|---|
| Furos internos profundos | Os pinos são mais fáceis de moer com precisão |
| Características finas e sem suporte | Os pinos reduzem a complexidade da usinagem |
| Moldagem de resina de alto desgaste | Pinos gastos podem ser trocados rapidamente |
| Cronomes de manutenção rigorosos | Reparos levam menos tempo de inatividade |
Muitas oficinas associam sistemas de pinos centrais com outros componentes substituíveis, como Sistemas de pinos de molde to simplify long-term mold maintenance.
Which core pin materials work best for different molding conditions?
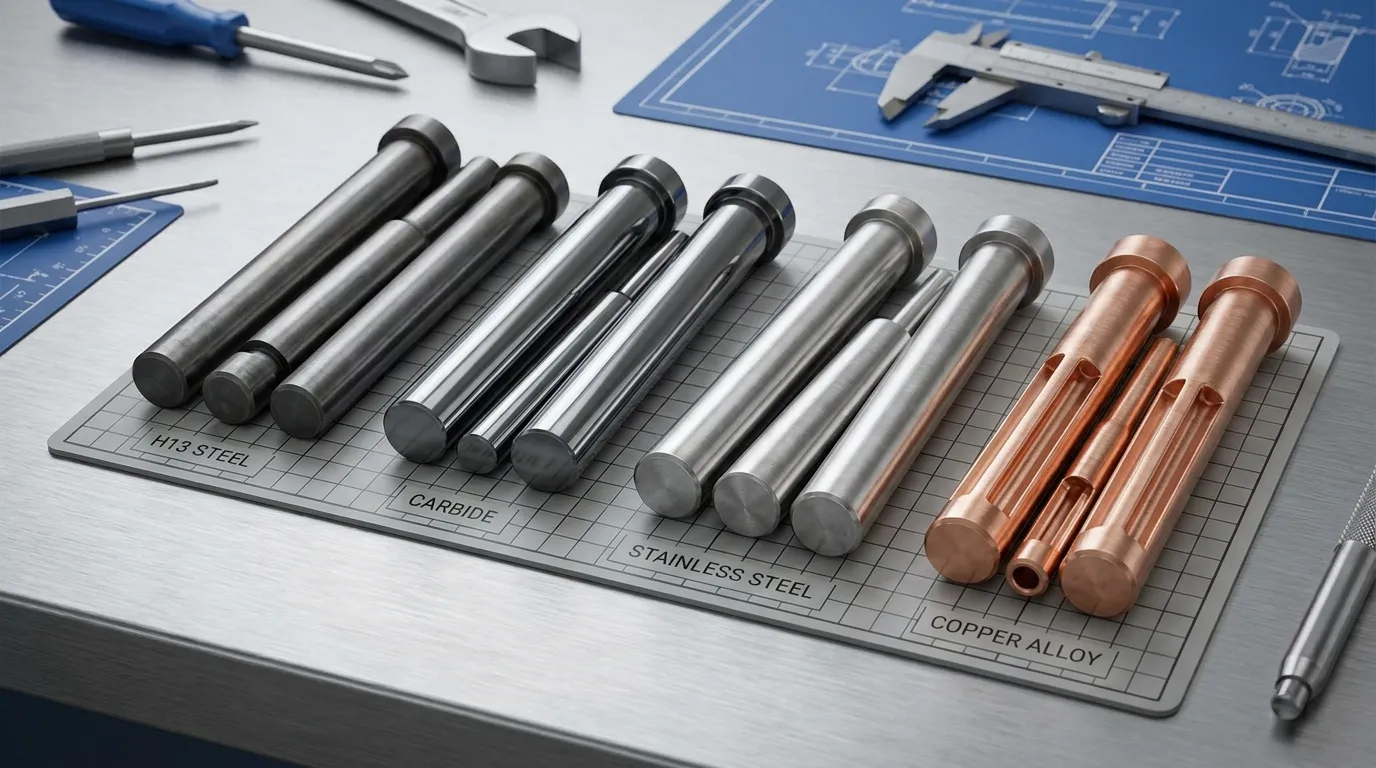
H13 steel works well for general-purpose molding, while carbide performs better in high-wear or ultra-tight tolerance applications. Copper-alloy core pins improve heat transfer in difficult cooling zones but may trade off wear resistance.
Material selection depends on resin type, Volume do ciclo, dimensional tolerance, and heat management. Most injection molds use hardened tool steel because it balances toughness and wear resistance. High-abrasion applications often require stronger materials.
A mold running glass-filled nylon creates more wear than a standard polypropylene part. In that situation, carbide may last longer than standard H13 steel. Carbide is not always the best choice, embora. Melhora a resistência ao desgaste, but brittle failure risk increases in unsupported or impact-prone designs.
Quando os pinos de núcleo de carboneto fazem sentido
Carbide core pins are commonly used in medical, Eletrônica, and connector molds that require extremely small diameters or very high cycle counts. A medical connector mold with multiple micro-holes may rely on carbide to maintain hole consistency over long production runs.
Long unsupported carbide pins can still crack under stress. For molds with impact loading or alignment variation, hardened tool steel is often safer.
| Material | Melhor Uso | Resistência ao desgaste | Transferência de Calor | Custo Relativo |
|---|---|---|---|---|
| Aço para ferramentas H13 | Moldagem de uso geral | Alto | Moderado | Médio |
| Aço inoxidável | Ambientes corrosivos | Moderado | Moderado | Médio |
| Carbeto | Resina abrasiva, micro features | Muito alto | Baixo | Alto |
| Liga de cobre | Áreas críticas de resfriamento | Moderado | Muito alto | Alto |
Some manufacturers also use specialty heat-transfer alloys for difficult cooling zones. Pinos de desempenho do núcleo PCS highlight this approach for reducing cycle time in thick-section molds.
For related component materials, see this guide to Materiais de pinos de precisão.
What tolerances and surface finishes are realistic for core pins?
Precision core pins are commonly manufactured to micron-level tolerances for medical, Eletrônica, and connector molds. Surface finish and concentricity directly affect molded hole quality, flash control, and part release performance.
Tolerance requirements depend on the molded feature, Retração da resina, and part function. A simple consumer product may tolerate larger variation than a medical connector or electronic housing. Tight-tolerance molds often require precision grinding and polishing to maintain consistent internal geometry.
Surface finish also matters. Rough pin surfaces can create drag during ejection or leave marks inside the molded hole. Polished finishes reduce friction and improve release consistency.
| Requisito de Recursos | Prioridade típica de pinos de núcleo |
|---|---|
| Diâmetro de furo apertado | Tolerância de diâmetro |
| Parede interna lisa | Acabamento superficial |
| Característica cilíndrica profunda | Retidão |
| Alinhamento de alta precisão | Concensicidade |
Using extremely tight tolerances is not always beneficial. Over-specifying precision can increase machining cost without improving molded part performance. Buyers should match tolerance targets to actual application needs instead of defaulting to the smallest possible numbers.
A consumer electronics mold may require a polished pin to avoid cosmetic marks. A structural automotive bracket often prioritizes durability and wear resistance instead. Suppliers such as Precisão Solar emphasize precision grinding and dimensional consistency because small tolerance variation can affect molded part fit and assembly.
When do standard core pins stop working?
Standard catalog core pins work for many molds, but custom pins become necessary when designs require unusual diameters, long unsupported lengths, aggressive resins, or advanced cooling performance.
Standard pins reduce lead time and simplify sourcing. They work well for common diameters and standard molding conditions. Problems appear when molded geometry becomes more specialized.
A deep cylindrical feature with a very small diameter may require custom support geometry or advanced material selection. Electronics molds often need tiny precision pins that standard catalogs do not cover.
Sinais de que um molde precisa de pinos de núcleo personalizados
- Geometria de diâmetro ou ponta não padrão
- Resina abrasiva, como o nylon preenchido com vidro
- Comprimento longo do núcleo sem suporte
- Tolerâncias estéticas ou médicas rigorosas
- Seções grossas sensíveis ao resfriamento
Using standard catalog pins can reduce cost upfront, but forcing standard dimensions into complex molds often creates maintenance problems later. Some manufacturers solve this by ordering custom-machined mold components built for the exact application.
Empresas como Fornecedores do IPros offer non-standard configurations for molds that exceed catalog limitations. Related custom accessories such as Acessórios personalizados para moldes are also common in specialized tooling systems.
How are precision core pins manufactured?
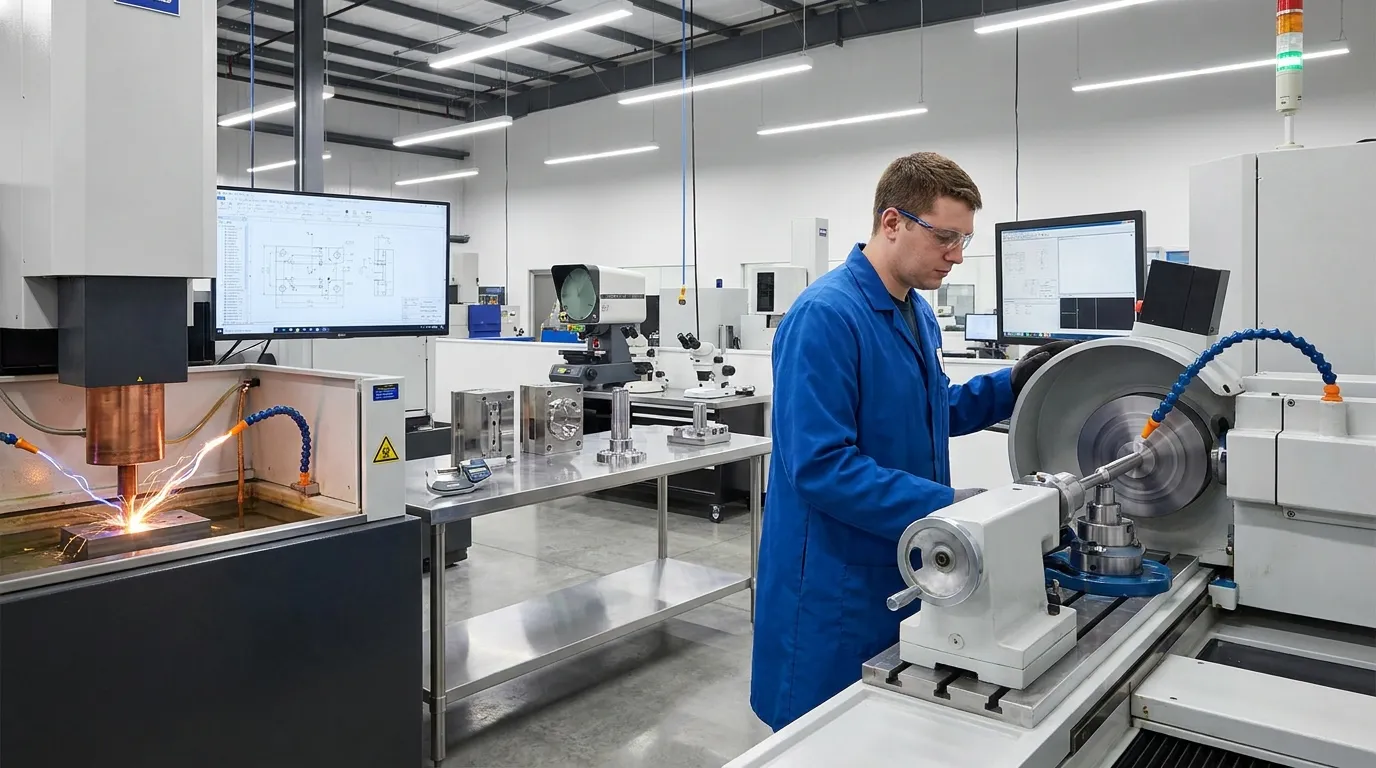
High-precision core pins are typically produced through grinding, Tratamento térmico, Usinagem EDM, and precision polishing. Manufacturing consistency matters because even small dimensional variation can affect molded hole accuracy and mold life.
Most core pins start as hardened tool steel or carbide stock. Manufacturers machine the rough geometry first, then use grinding and polishing operations to achieve final dimensions and surface finish. Precision grinding is especially important for small-diameter pins.
Por que o tratamento térmico importa
Heat treatment increases hardness and wear resistance. Poor heat treatment can leave pins brittle or dimensionally unstable. Some manufacturers heat-treat before finish grinding to reduce distortion during final machining.
Electrical discharge machining (EDM) is common for detailed tip geometry or difficult shapes. EDM removes material with electrical sparks instead of cutting tools, making it useful for precision mold work.
| Etapa de Fabricação | Propósito |
|---|---|
| Usinagem bruta | Cria geometria básica |
| Tratamento térmico | Melhora a dureza |
| Rectificação de precisão | Atinge a tolerância final |
| Usinagem EDM | Produz detalhes complexos |
| Polimento | Improves surface finish |
A medical mold with ultra-small internal holes may require multiple grinding and polishing passes before approval. In electronics tooling, even slight dimensional drift can cause connector alignment problems during assembly.
Machining consistency also affects maintenance intervals. Shops producing Usinagem de componentes de molde systems often focus heavily on grinding accuracy because repeatability matters as much as the original tolerance.
What causes core pin wear, Dobra, or failure?
Most core pin failures come from poor support, Materiais abrasivos, Tensão térmica, ou problemas de alinhamento. Small-diameter pins are especially vulnerable when long unsupported lengths create bending stress during molding cycles.
Wear usually appears gradually. Abrasive resins can round edges or reduce dimensional accuracy over time. Bending and breakage are more severe because they can stop production immediately.
A long unsupported pin inside a deep cylindrical cavity experiences repeated stress during injection pressure and ejection. If the diameter is too small, the pin may flex slightly during every cycle until fatigue causes failure.
| Sintoma de falha | Causa Provável | Método de Prevenção |
|---|---|---|
| Curvação de pinos | Comprimento excedente sem suporte | Adicionar suporte ou aumentar o diâmetro |
| Desgaste superficial | Resina abrasiva | Use carboneto ou pino revestido |
| Rachaduras | Tensão térmica | Melhorar o equilíbrio de resfriamento |
| Clarão ao redor do buraco | Acabamento superficial desgastado | Remoagem ou substituição do pino |
An electronics housing mold may start showing flash around screw holes after the pin surface wears down. In automotive molding, unsupported thin pins can gradually bend during long production runs.
Regular inspection helps prevent unplanned downtime. Many mold shops combine core pin maintenance with broader Prevenção de desgaste por mofo programs to catch alignment or wear issues early.
How should buyers specify core pins to suppliers?
Buyers should provide clear dimensional, Material, and performance requirements before production begins. Incomplete specifications often lead to tolerance issues, short mold life, or mismatched materials.
A strong specification package should include:
- Diâmetro e comprimento do pino
- Requisitos de tolerância
- Expectativas de acabamento superficial
- Tipo de resina e condições de moldagem
- Necessidades de resfriamento ou transferência de calor
- Volume de produção esperado
Application details matter more than many buyers expect. A supplier choosing material for a polypropylene consumer product may recommend something very different from a glass-filled nylon automotive mold.
Por exemplo, a medical connector mold requiring ultra-small holes may need carbide pins with polished finishes and strict concentricity control. A high-volume automotive bracket mold may prioritize toughness and wear resistance instead.
For a broader look at molding systems and production strategy, isso Guia de molde de injeção plástica covers how mold components fit into the full tooling process.
Como Escolher a Opção Certa
The best core pins balance precision, Durabilidade, Desempenho de resfriamento, and maintenance practicality. Material choice alone will not solve a poor support design or unrealistic tolerance target. Buyers should evaluate the molded feature, Tipo de resina, Volume do ciclo, and maintenance expectations together before finalizing specifications.
Standard pins work well for many applications, but custom solutions often make sense for thin walls, Resinas abrasivas, or precision internal geometry. A well-designed core pin system reduces downtime, improves molded part consistency, and extends overall mold life. If you are reviewing a new tooling project, start with the molded feature requirements first, then build the core pin specification around real production conditions.
Perguntas Frequentes
Qual é a diferença entre um pino central e um pino ejetor?
A core pin forms internal features in the molded part, while an ejector pin pushes the finished part out of the mold after cooling. Many molds use both systems together, but they perform different functions during the molding cycle.
What material is commonly used for core pins?
H13 tool steel is one of the most common materials because it balances hardness, Resistência, e resistência ao calor. Carbide and stainless steel are also used for abrasive resins, corrosive molding conditions, and high-precision applications.
Why do core pins break?
Core pins usually fail because of poor support, excessive length-to-diameter ratio, Tensão térmica, or abrasive resin wear. Small-diameter pins are especially vulnerable when repeated molding cycles create bending fatigue over time.
Can core pins be custom made?
Sim. Custom core pins are widely used for unusual diameters, deep internal features, Tolerâncias Apertadas, or advanced cooling requirements that standard catalog components cannot support effectively.
How precise are injection mold core pins?
Precision core pins can be manufactured to micron-level tolerances depending on the application. Medicina, Eletrônica, and connector molds often require tighter dimensional control and higher surface finish quality than general consumer products.
Are carbide core pins better than steel?
Carbide core pins offer excellent wear resistance and dimensional stability in abrasive molding applications. They are also more brittle and expensive than hardened tool steel, so they are not always the safest choice for unsupported designs.
Compartilhe:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
