



Mangas ejetora: Quando usá-los em vez de pinos ejetores
Ejector sleeves are used in injection molds when parts eject around a core pin, deep boss, or cylindrical feature where standard ejector pins cannot distribute force evenly. They improve concentric ejection, reduce cosmetic defects, and protect hollow or thin-wall features. Correct sleeve fit, Autorização, and concentricity are critical because poor alignment increases wear, Fixação, and part damage during ejection.
Parts with deep bosses or tall cylindrical cores often fail when standard ejector pins apply uneven force during ejection. That problem gets worse in cosmetic molds where stress marks or cracking can ruin the finished part. Ejector sleeves solve this by distributing force around the feature instead of pushing from one small point. The challenge is knowing when sleeves are necessary, how tight the fit should be, and what specifications matter before production starts.
What does an ejector sleeve do in injection molding?
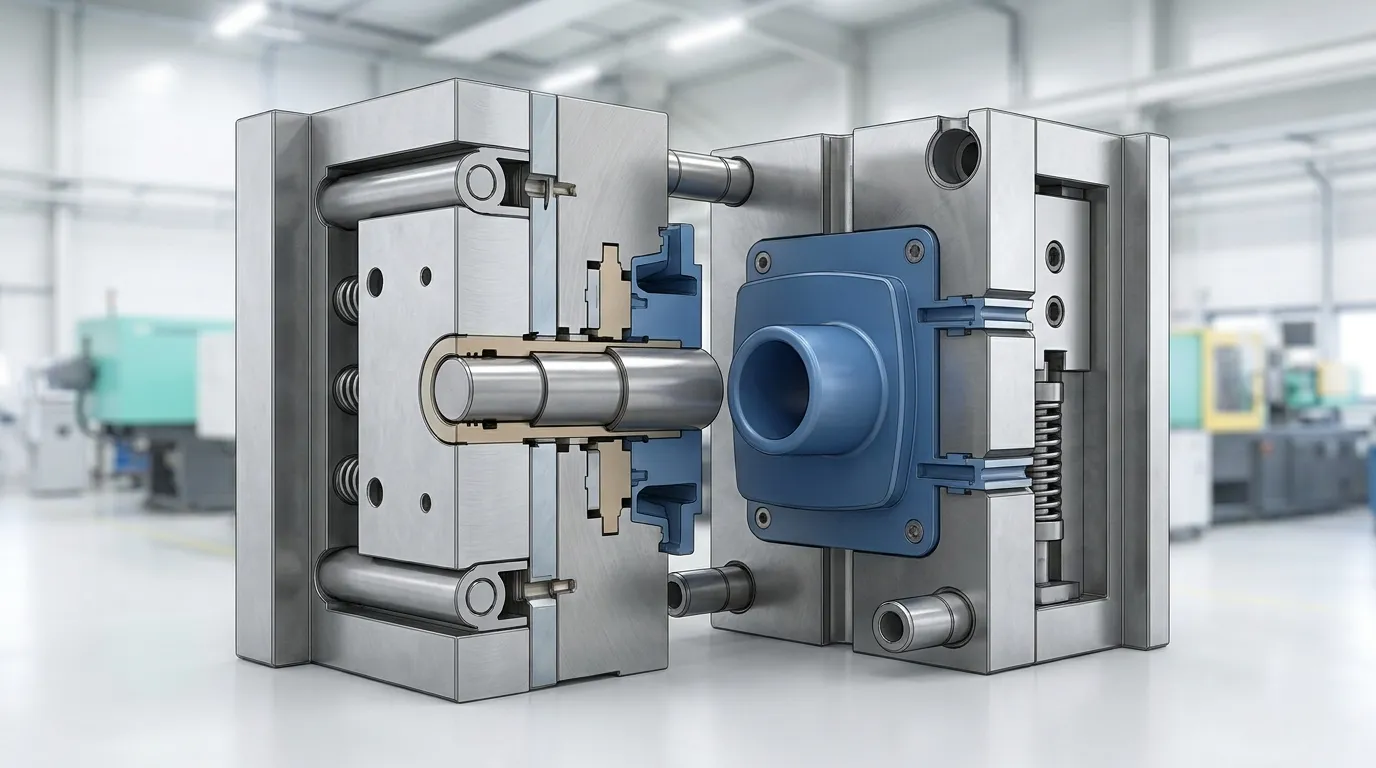
Ejector sleeves are tubular ejectors designed to push molded parts off core pins or cylindrical features evenly. They reduce stress concentration compared to standard ejector pins and help prevent deformation around bosses or hollow sections.
An ejector sleeve works like a hollow ejector pin. Instead of pushing from a single contact point, the sleeve surrounds the core pin and applies force evenly around the molded feature. This helps the part release without tilting, rachaduras, or sticking during ejection.
Sleeves are commonly used for cylindrical geometries such as bosses, hubs, e seções ocas. These shapes often trap tightly around the core pin after cooling. A standard pin can create localized stress in one area, especially on thin-wall plastic parts.
De acordo com o US5730812A patente de fabricação, ejector sleeves are produced with strict concentricity control so the sleeve moves smoothly around the core pin during repeated molding cycles.
For readers who want a broader overview of mold components, Sunshine Pro Guia completo de componentes do molde explains how ejector systems fit into the full mold assembly.
Você também pode revisar esses Fundamentos do pino ejetor to compare solid pins with sleeve-style ejectors.
When should you use an ejector sleeve instead of an ejector pin?
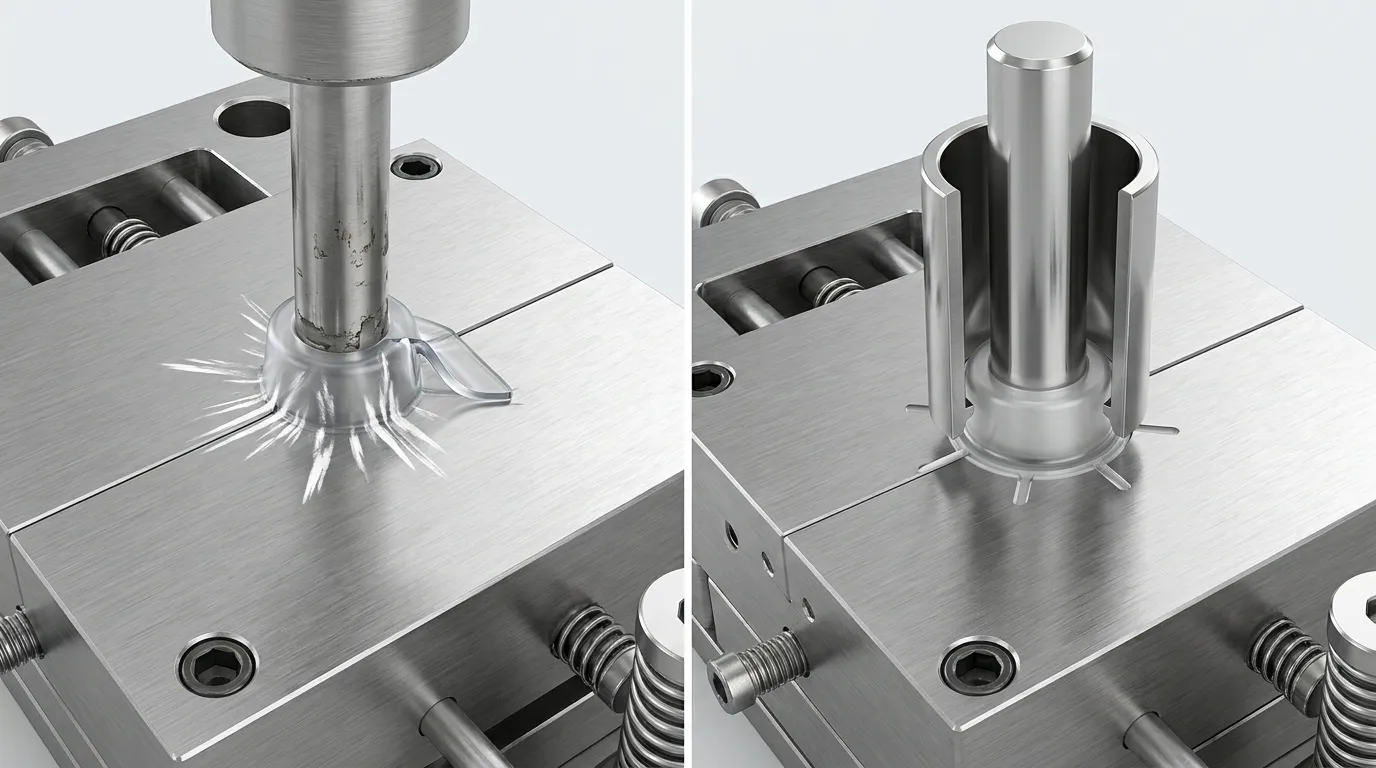
Use ejector sleeves when parts eject around a core pin, deep boss, or cylindrical feature where a standard ejector pin would create uneven force or visible stress marks. Sleeves distribute pressure more evenly and improve concentric ejection.
Ejector sleeves are usually the safer choice when the molded feature surrounds a core pin. The sleeve keeps the ejection force centered, which reduces side loading and lowers the risk of deformation. This matters most in cosmetic parts, thin-wall parts, and deep cylindrical geometries.
Standard ejector pins are not automatically the simpler or safer option. Around deep bosses or cylindrical cores, they often create uneven force that increases cosmetic defects and sticking risk. A sleeve may cost more upfront, but it can prevent expensive mold adjustments later.
Tabela de Decisão de Sleeve vs Pin
| Geometria das Peças | Opção Recomendada | Risco se a escolha errada for usada | Sensibilidade Estética |
|---|---|---|---|
| Chefe profundo | Manga ejetora | Quebrar chefes | Alto |
| Cilindro oco | Manga ejetora | Liberação desigual | Alto |
| Área estrutural plana | Pino ejetor | Risco mínimo | Baixo |
| Recurso suportado por núcleos altos | Manga ejetora | Carregamento lateral | Médio |
| Parede espessa não estética | Pino ejetor | Marcas menores de testemunha | Baixo |
A cosmetic electronics housing is a common example. Deep screw bosses inside the housing often show stress whitening when standard pins eject too aggressively from one side. A sleeve spreads the force around the boss and reduces visible defects.
For a broader look at mold ejection layouts, Guia do Sunshine Pro para Projeto do sistema de ejeção explains how different ejector components work together inside the mold.
Which molded part geometries typically require ejector sleeves?
Ejector sleeves are commonly used for deep bosses, cylindrical hubs, and hollow molded sections where centered ejection is critical. These geometries often fail with standard pins because force concentrates on a small contact area.
Most sleeve applications involve parts that wrap tightly around a cylindrical core. During cooling, the plastic shrinks around the core pin, which increases friction during ejection. A centered sleeve helps release the part evenly instead of pushing from one edge.
Common examples include bottle caps, medical housings, electronic screw bosses, and precision cylindrical parts. High-cycle cap molds often rely on sleeves because the parts are thin, flexible, and sensitive to deformation during release.
Aplicações Comuns em Geometria
| Tipo de Geometria | Por que as mangas ajudam |
|---|---|
| Chefes profundos | Evita rachaduras ao redor da parede do chefe |
| Tampas de parede fina | Reduz a deformação durante a liberação |
| Cubos cilíndricos | Mantém a ejeção concêntrica |
| Alojamentos cosméticos | Reduz marcas visíveis de estresse |
| Peças altas suportadas por núcleo | Previne o carregamento lateral |
Por que as mangas são comumente usadas ao redor dos pinos do núcleo
Core pins support internal molded features such as holes, Chefes, and tubes. When the plastic cools, those features grip the core tightly. An ejector sleeve moves around the core pin and applies balanced pressure to the entire feature.
De acordo com ZJ Mould Tech, sleeve ejectors are widely used for cylindrical molding applications because they improve ejection stability around core-supported geometries.
Você também pode revisar esses Componentes de ejeção de mofo to understand where sleeves fit inside larger ejection assemblies.
Why do fit and concentricity matter for ejector sleeves?
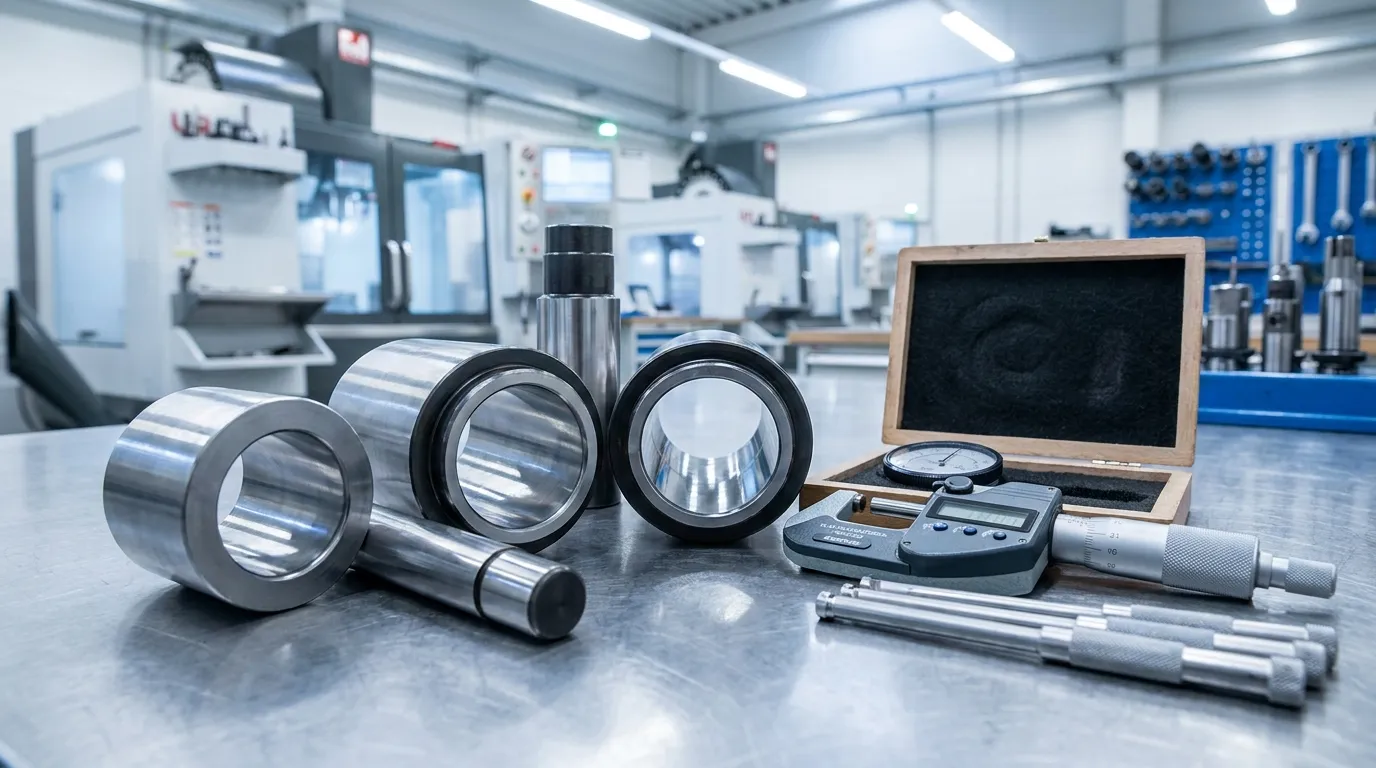
Ejector sleeves require tight concentricity and controlled clearance because misalignment increases friction, Desgaste, and sticking during ejection. Poor fit can damage both the molded part and the mold core.
Unlike standard ejector pins, sleeves move around another component. That means both the inside diameter and outside diameter must stay aligned during repeated molding cycles. Even small concentricity errors can create uneven contact and friction.
O Especificações da manga ejetora Choice Mold reference tight TIR values and nitrided surfaces to improve alignment stability and wear resistance. Those tolerances become more important in high-cycle molds.
Overly tight sleeve clearance is not always better. Tight fits improve stability, but aggressive clearance reduction can increase galling and friction if lubrication or alignment is poor. In many production molds, controlled movement is safer than forcing near-zero clearance.
Problemas comuns causados por baixa concentricidade
| Problema | Causa Provável |
|---|---|
| Encadernação de mangas | Pino do núcleo desalinhado |
| Irritação | Atrito excessivo |
| Desgaste desigual | Pouca concentricidade |
| Fixação de peças | Folga apertada |
| Dano no núcleo | Carregamento lateral durante a ejeção |
A medical molding application is a good example. Medical molds often run high volumes with strict dimensional requirements. Many manufacturers use nitrided sleeves because the harder surface helps reduce wear while maintaining stable movement around the core pin.
What materials and surface treatments are commonly used for ejector sleeves?
Most ejector sleeves use H13 or SKD61 hot-work tool steel because these materials resist wear, thermal fatigue, and repeated ejection stress. Nitrided surfaces further improve hardness and reduce galling.
Injection molds run through repeated heating and cooling cycles, so sleeve materials must resist thermal fatigue and surface wear. H13 and SKD61 are common choices because they hold hardness well under high-temperature production conditions.
De acordo com Visão geral do material do ZGCGMJ, SKD61 provides strong wear resistance and thermal stability for repeated molding cycles. Many suppliers also add nitriding treatments to increase surface hardness without making the sleeve brittle.
Materiais comuns das mangas ejetora
| Material | Principal benefício | Uso típico |
|---|---|---|
| Aço H13 | Resistência ao calor | Moldes de alto ciclo |
| SKD61 | Resistência ao desgaste | Moldes de precisão |
| Aço nitrutrado | Dureza superficial | Peças cosméticas |
| Aço para ferramentas endurecido | Durabilidade | Produção geral |
A thin-wall cap mold running continuously at high speed puts heavy wear on sleeve surfaces. In that situation, nitrided sleeves often last longer because the hardened surface reduces friction during repeated ejection cycles.
What failures happen when the wrong ejector method is used?
Using ejector pins where sleeves are required can create uneven ejection force, leading to boss cracking, Marcas de tensão, Fixação, or deformation. Incorrect sleeve fit can also accelerate mold wear and cause galling.
Most ejection failures start with uneven force distribution. When a pin pushes against one side of a deep boss, the plastic can flex or crack during release. Cosmetic surfaces are especially vulnerable because stress whitening often appears before the part fully ejects.
A mold with poor sleeve concentricity can create another problem. Repeated friction between the sleeve and core pin causes galling, which is surface damage created by metal-to-metal contact. Once galling starts, the sleeve movement becomes rough and sticking gets worse.
Falhas comuns de ejeção
| Fracasso | Causa Típica | Solução Melhor |
|---|---|---|
| Clareamento por estresse | Força irregular dos pinos | Uso da ejeção da manga |
| Quebrar chefes | Carregamento lateral | Força da manga centralizada |
| Irritação | Limpeza ruim | Ajuste correto e lubrificação |
| Fixação de peças | Desalinhamento | Melhorar a concentricidade |
| Desgaste desigual | Controle de tolerância frouxo | Ajuste de manga de precisão |
O Fabricação de moldesAnálise tecnológica highlights how wear conditions and improper operating alignment contribute to ejector sleeve failure over time.
Você também pode revisar esses Problemas comuns com pinos ejetores to understand how poor ejection choices affect overall mold performance.
How do you specify ejector sleeves correctly for a mold build?
Correct ejector sleeve specification depends on core-pin diameter, required clearance, stroke length, Dureza, and concentricity tolerance. Inaccurate sizing increases wear risk and can create unstable ejection.
The first step is matching the sleeve ID to the core pin diameter with the correct running clearance. The sleeve must move freely without excessive looseness. Stroke length also matters because the sleeve needs enough travel to release the molded feature completely.
Standard catalog sleeves work for many molds, but complex cosmetic parts often require custom dimensions or tighter concentricity controls than off-the-shelf components provide. Buyers sometimes underestimate how much part geometry affects sleeve specification.
Lista de Verificação de Especificação da Manga Ejetora
| Item de especificação | Por que isso importa |
|---|---|
| Diâmetro do pino do núcleo | Determina o ID da manga |
| Sleeve OD | Encaixa no layout da placa ejetora |
| Ajuste de folga | Controle a estabilidade do movimento |
| Comprimento do curso | Garante a ejeção total |
| Grau de material | Afeta a vida útil do desgaste |
| Dureza | Melhora a durabilidade |
| Tratamento superficial | Reduz a galha |
| Tolerância à concencicidade | Previne a entravamento |
Quando uma manga ejetora personalizada é necessária
Custom sleeves are often required for unusual boss geometries, cosmetic molds, or precision medical parts. A standard sleeve may fit dimensionally but still fail if the tolerance stack creates unstable movement around the core.
A procurement comparison shows this clearly. A standard MISUMI sleeve may work for a common bottle-cap mold, but a custom-machined sleeve is often safer for a nonstandard electronics housing with tight cosmetic requirements.
For more detail on precision component sizing, Guia do Sunshine Pro para Tolerâncias de ferramentas de precisão explains how tolerance control affects tooling performance.
Are standard ejector sleeves enough for most molds?
Standard ejector sleeves handle many production molds successfully, especially for common cylindrical geometries with moderate cosmetic requirements. They are easier to source, less expensive, and available in common dimensions from major suppliers.
Custom sleeves become more important when molds require unusual diameters, tighter concentricity, or higher cosmetic standards. Medical molds, thin-wall packaging, and precision electronics often need tighter control than standard catalog parts provide.
Mangas padrão vs personalizadas
| Fator | Manga Padrão | Sleeve Personalizado |
|---|---|---|
| Prazo de entrega | Curta | Mais tempo |
| Custo | Lower | Mais alto |
| Tamanhos disponíveis | Limitado | Flexível |
| Controle de concentricidade | Grau padrão | Aplicação específica |
| Desempenho cosmético | Moderado | Maior precisão |
If the mold uses basic cylindrical features and standard production speeds, catalog sleeves are usually enough. For high-cycle or cosmetic molds, tighter engineering control often pays for itself through lower defect rates and reduced maintenance.
Como Escolher a Opção Certa
Choosing between ejector sleeves and standard pins comes down to geometry, force distribution, and tolerance control. Chefes profundos, cylindrical cores, and cosmetic surfaces usually benefit from sleeve ejection because the force stays centered during release.
Before finalizing a mold design, review the core-pin diameter, clearance fit, Volume de produção esperado, e requisitos cosméticos. Those details affect wear life more than the component price alone. When ejector sleeves are specified correctly, they reduce sticking, Melhorar a qualidade das peças, and help stabilize long production runs.
Perguntas Frequentes
What is the primary function of an ejector sleeve?
An ejector sleeve pushes molded parts evenly around a core pin or cylindrical feature during mold ejection. It spreads force over a larger contact area than a standard ejector pin, which helps reduce stress marks and deformation.
When should ejector sleeves be used instead of ejector pins?
Ejector sleeves should be used for deep bosses, hollow cylinders, and core-pin-supported features that require centered ejection. Standard ejector pins can apply uneven pressure and increase the risk of cracking or visible stress marks.
Why are ejector sleeves used around core pins?
Ejector sleeves surround the core pin so the ejection force stays balanced around the molded feature. This reduces side loading, improves release stability, and helps prevent sticking during production.
What materials are commonly used for ejector sleeves?
H13 and SKD61 hot-work tool steels are common ejector sleeve materials because they resist wear and thermal fatigue. Many manufacturers also use nitrided surfaces to improve hardness and reduce galling.
What causes ejector sleeve failure?
Pouca concentricidade, incorrect clearance, lubrificação inadequada, and side loading are common causes of ejector sleeve failure. These conditions increase friction and wear, which can lead to binding and unstable ejection.
Do ejector sleeves require tight tolerances?
Sim, ejector sleeves require controlled clearance and tight concentricity so they move smoothly around the core pin. Loose or misaligned sleeves increase wear and can damage both the mold and molded part.
Compartilhe:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
