



Plastic Injection Mold Design: DFM Checklist for Stronger Plastic Parts
Plastic injection mold design depends on good DFM decisions before tooling starts. Consistent wall thickness, Ângulos de tiragem adequados, balanced ribs, smooth corner transitions, and clean ejection planning help prevent sink marks, Deformação, Chutes curtos, and mold wear. A practical DFM checklist reduces tooling revisions, improves part strength, and helps manufacturers move into production with fewer delays and quality problems.
A plastic part can look perfect in CAD and still fail during production. Small geometry choices often create sink marks, ejection problems, or expensive tooling changes once steel cutting begins. That’s why DFM, Abreviação de Design for Manufacturability, matters early. This guide walks through the key checks engineers use before approving a plastic part for injection molding, with practical examples you can apply before sending a design to tooling.
What is plastic injection mold design and why does DFM matter?
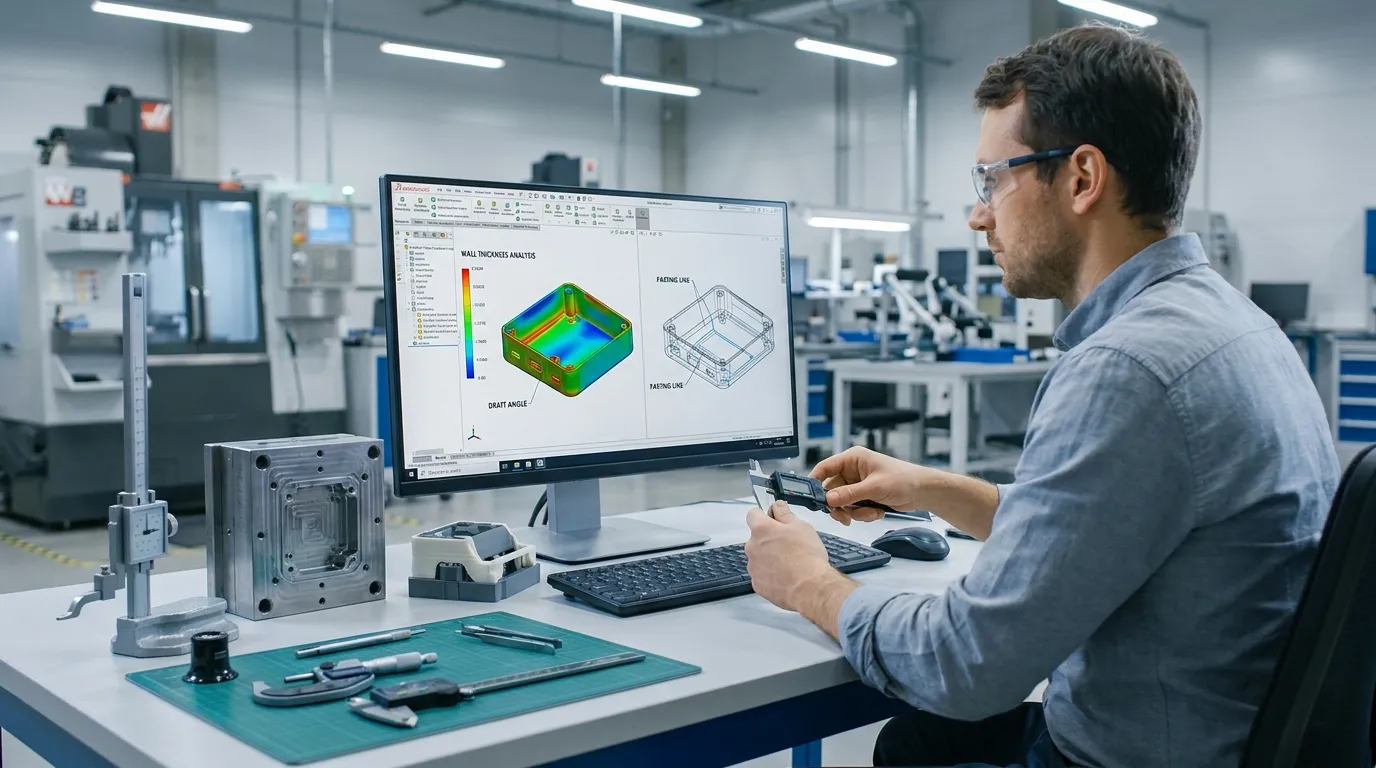
Plastic injection mold design works best when DFM decisions happen before tooling starts. Espessura da parede, draft, costelas, and ejection features directly affect defects, Tempo do ciclo, Complexidade das ferramentas, e consistência de partes.
Plastic injection mold design is the process of shaping a part so it can be manufactured reliably inside an injection mold. DFM focuses on reducing production risks before the mold is machined. De acordo com CustomPartNet, geometry choices directly affect cooling behavior, encolhimento, and defect risk during molding.
A strong DFM review looks beyond appearance. Engineers check whether plastic can flow evenly, cool consistently, and eject cleanly from the mold. Even small changes to wall transitions or rib placement can improve part quality and reduce tooling revisions later.
Many product teams wait too long to review manufacturability. That usually increases cost because mold modifications after steel cutting are slower and more expensive than CAD updates early in development.
- Are wall sections consistent?
- Does every vertical face include draft?
- Are ribs sized correctly?
- Will the part eject without scuffing?
- Are undercuts necessary?
Se você precisa de uma visão geral mais ampla das ferramentas, Revise isso Fundamentos do projeto de moldes por injeção guide before moving into detailed DFM checks.
What wall thickness works best for injection molded parts?
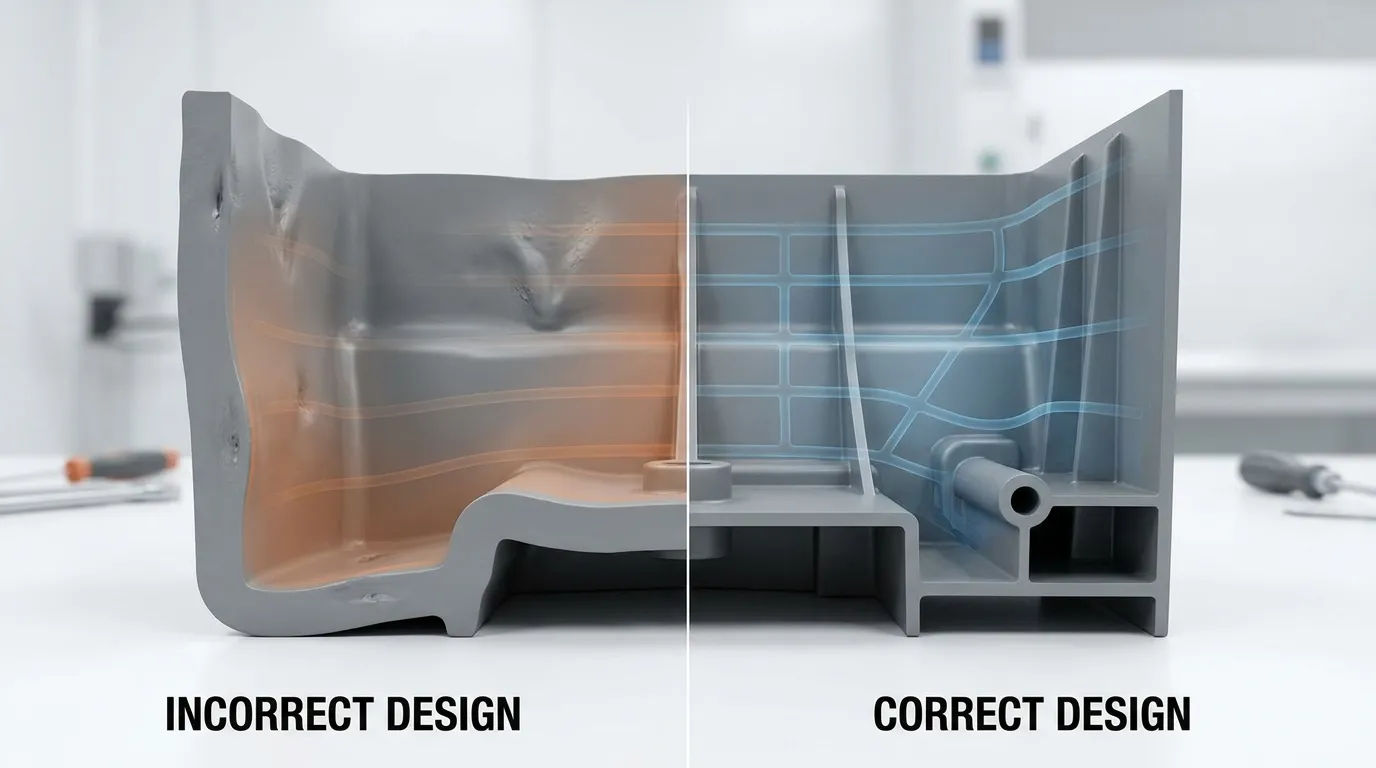
Consistent wall thickness improves plastic flow, cooling balance, e estabilidade dimensional. Thick sections often create sink marks and warping, while abrupt thickness changes increase internal stress and molding defects.
Wall consistency matters more than maximum thickness. Plastic shrinks as it cools, and uneven cooling creates distortion. Thick sections hold heat longer than thin sections, which increases the risk of sink marks and warped geometry.
A common mistake is adding extra wall thickness to improve strength. Thick walls are not always the best solution. Em muitos casos, properly designed ribs create better stiffness with fewer molding defects.
A handheld electronics housing is a good example. One design used ribs that matched full wall thickness. During molding, the rib area cooled unevenly and created visible sink marks on the outer cosmetic surface. Reducing rib thickness solved the issue without reducing strength.
What causes sink marks in thick wall sections?
Sink marks happen when thicker areas shrink more during cooling. Costelas sobredimensionadas, Chefes, and sudden wall transitions usually create the biggest problems.
| Condição de Projeto | Resultado Provável | Melhor Abordagem |
|---|---|---|
| Seções grossas de parede | Marcas de afundamento | Mantenha a espessura da parede consistente |
| Transição repentina da parede | Estresse interno | Use transições graduais |
| Nervelas de espessura total | Distorção superficial | Use nervuras de reforço mais finas |
| Massa pesada de canto | Resfriamento desigual | Adicionar raios de canto |
Isso Considerações de design de moldes resource explains how geometry affects manufacturability across different tooling situations.
Why are draft angles critical for clean part ejection?
Draft angles help molded parts release from the tool without dragging or surface damage. Even small draft improvements can reduce ejection force, Defeitos cosméticos, and mold wear during high-volume production.
Draft creates a slight taper on vertical surfaces so parts can separate from the mold during ejection. Without draft, the plastic drags against the mold wall and increases friction during release.
Zero-draft walls may look acceptable in CAD, but they often create real production problems. Surface scratching, Fixação, and ejector stress become more common as cycle counts increase. Protolabs notes that manufacturable geometry improves production consistency and tooling efficiency.
Textured surfaces need even more draft because texture increases contact area inside the mold. A medical enclosure with textured side walls experienced repeated ejection scratches during production testing. Adding draft solved the issue without changing the product appearance.
- Adicione corrente de ar em todas as paredes verticais
- Aumentar o rascunho em superfícies texturizadas
- Verifique cuidadosamente as costelas profundas
- Revise as localizações dos ejetores cedo
- Evite cantos internos afiados
For tight-tolerance products, isso Tolerâncias de moldagem de precisão guide explains how geometry affects dimensional accuracy.
How should ribs and bosses be designed for strength without defects?
Ribs improve stiffness without increasing overall wall thickness when they are properly proportioned. Oversized ribs or unsupported bosses commonly create sink marks, cosmetic distortion, and uneven cooling.
Ribs are one of the safest ways to strengthen a plastic part. They improve stiffness without adding excessive material mass. The key is controlling rib dimensions so cooling remains balanced.
Many cosmetic defects come from oversized ribs hidden behind visible surfaces. Engineers often assume thicker ribs mean stronger parts, but oversized reinforcement usually creates more shrinkage problems during cooling.
Diretrizes de espessura das nervuras
A practical rule is keeping rib thickness smaller than the surrounding wall section. Balanced geometry improves cooling and reduces visible surface distortion.
| Característica | Prática Recomendada | Risco se Ignorado |
|---|---|---|
| Espessura das nervuras | Mais fina que a parede principal | Marcas de afundamento |
| Altura das costelas | Proporção de aspecto moderada | Problemas de preenchimento |
| Espaçamento das nervuras | Espaçamento uniforme | Retração desigual |
| Cantos das nervuras | Adicionar raios | Concentração de tensão |
Erros no reforço do chefe
Bosses often fail because they are unsupported or connected to thick wall sections. A cosmetic packaging cap warped after molding because one side used a heavy reinforced boss design. Redistributing the support ribs balanced cooling and corrected the distortion.
Unsupported bosses can also crack during assembly. Adding gussets or connecting ribs usually improves durability without increasing overall wall thickness.
For complex molded components, isso Peças moldadas com precisão page shows how controlled geometry supports stable production quality.
Which part features increase mold complexity and tooling cost?
Undercuts, deep ribs, Cantos afiados, and inaccessible geometry often require more complex tooling. These features increase machining time, maintenance requirements, and mold cost while raising defect risk.
Some design features force the mold to include sliders, Levantadores, or deep core structures. These mechanisms increase mold complexity and usually extend lead time. De acordo com o Visão geral do processo de moldagem por injeção, mold geometry directly affects tooling structure and manufacturing difficulty.
Undercuts should only be used when the product function truly requires them. Many cosmetic undercuts add tooling complexity without improving product performance.
An appliance housing is a common example. A late-stage cosmetic undercut required additional side actions inside the mold. That change increased tooling cost and delayed production approval because the mold needed redesign work.
Tabela de Complexidade de Características vs Ferramentas
| Característica | Risco de Fabricação | Impacto no Custo | Alternativa Melhor |
|---|---|---|---|
| Undercut cosmético | Ações secundárias necessárias | Alto | Simplificar a geometria |
| Cantos agudos | Concentração de tensão | Médio | Adicionar raios |
| Costelas profundas e estreitas | Dificuldade de preenchimento | Médio | Nervuras reforçadas mais curtas |
| Bosses grossos | Marcas de afundamento | Médio | Suporte Gusset |
| Paredes de tiro zero | Problemas de ejeção | Médio | Adicionar redução do rascunho |
Isso Processo de Design de Ferramentas resource explains how geometry choices affect mold engineering decisions.
How do engineers review a plastic part before tooling approval?
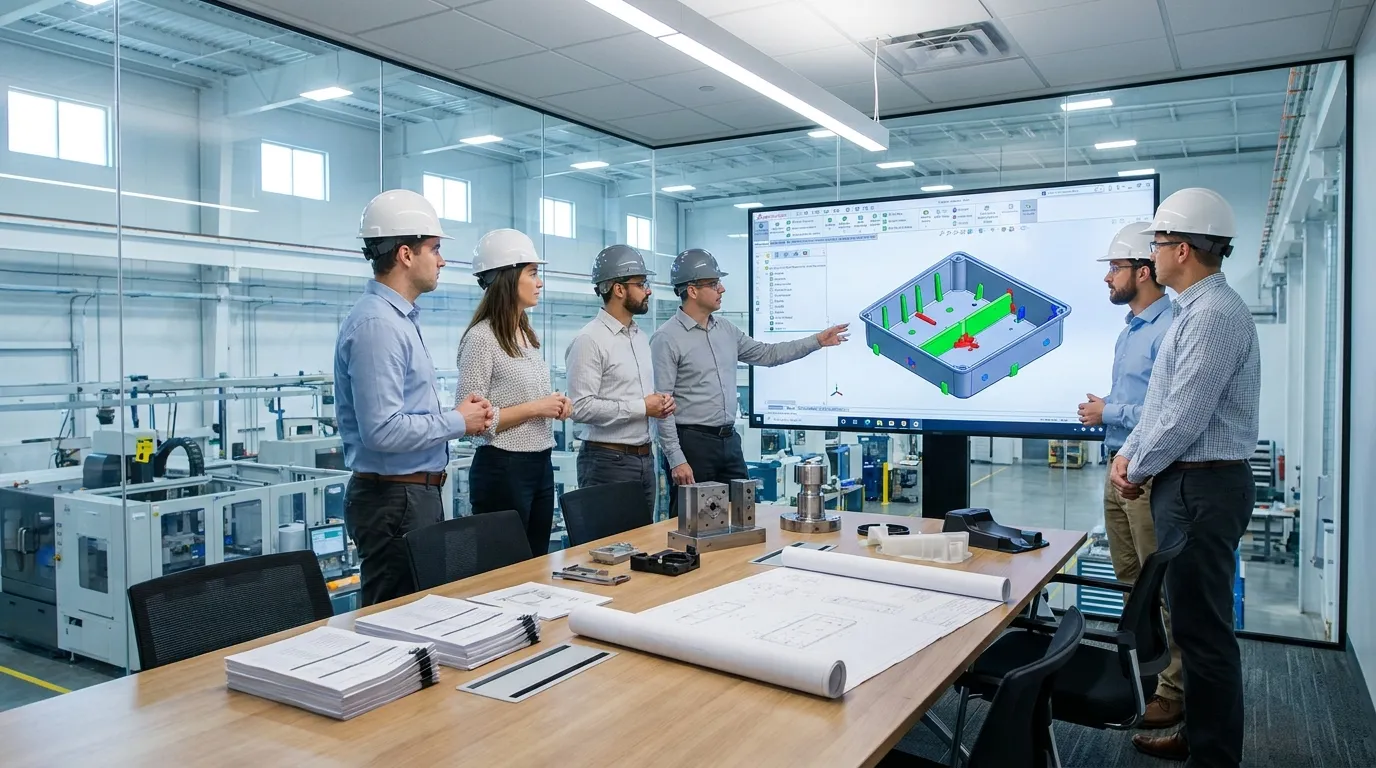
A proper injection molding DFM review checks wall consistency, draft, costelas, portões, parting lines, encolhimento, and ejection before steel cutting begins. Early corrections prevent expensive mold modifications later.
Most engineering teams follow a structured review before releasing tooling for machining. The goal is finding geometry risks before they become manufacturing delays.
A strong DFM process reviews the entire molding cycle, not just the CAD shape. Engineers evaluate how plastic fills the cavity, Cool, shrinks, and ejects during production.
Lista de verificação de DFM para pré-ferramentas
| Área da Lista de Verificação | O que os Engenheiros Avaliam |
|---|---|
| Espessura da parede | Consistência e zonas de transição |
| Draft | Folga de ejeção em todas as paredes verticais |
| Costelas e sombreiras | Razões de espessura e estrutura de suporte |
| Corners | Raio e concentração de tensão |
| Linha de despedida | Viabilidade da separação de mofo |
| Portões | Balanço de fluxo e impacto cosmético |
| Ejeção | Localização dos pinos e força de liberação |
| Undercuts | Necessidade de movimentos laterais ou levantadores de peso |
A product team manufacturing consumer electronics reduced tooling revisions by running this review before steel cutting. The team identified uneven wall transitions and corrected them in CAD instead of modifying hardened tooling later.
Many manufacturers also use mold flow analysis during this stage. Simulation helps identify filling problems, trapped air, and shrinkage risks before production begins.
For broader process planning, isso Fluxo de trabalho DFM guide covers additional mold engineering considerations.
If you need a larger manufacturing overview, a Guia completo de molde de injeção can help connect DFM decisions with the full tooling lifecycle.
What are the most common DFM mistakes in plastic part design?
Most molding defects come from a small group of repeat design mistakes. These problems usually appear during cooling, Ejeção, or dimensional inspection after production begins.
One of the most common mistakes is treating CAD appearance as proof of manufacturability. A part can look correct visually while still creating flow imbalance, Marcas de afundamento, or difficult ejection conditions inside the mold.
Tabela comum de solução de problemas de DFM
| Erro de Projeto | Problema de Produção | Solução Melhor |
|---|---|---|
| Sem corrente de ar | Travamento durante a ejeção | Adicionar ângulos de rascunho |
| Seções grossas de parede | Marcas de afundamento e empenamento | Manter a consistência da parede |
| Cantos internos agudos | Concentração de tensão | Adicionar raios |
| Costelas sobredimensionadas | Distorção cosmética | Reduzir a espessura das nervuras |
| Chefes sem suporte | Rachaduras durante a montagem | Adicione reforços ou canelas |
| Undercuts excessivos | Alto custo de ferramentas | Simplificar a geometria |
Isso Moldagem de alta precisão overview explains why small geometry adjustments matter for repeatable production quality.
Acertando o Próximo Passo
Good plastic injection mold design starts long before the mold is machined. Most production problems can be traced back to early geometry decisions involving wall thickness, draft, costelas, or ejection planning. A practical DFM review helps teams catch those risks while changes are still inexpensive.
Antes de aprovar ferramentas, review the part as a manufacturing engineer would. Check cooling behavior, ejection paths, reinforcement geometry, and mold complexity together. Small adjustments during design often prevent major tooling revisions later and help production move faster with fewer defects.
Perguntas Frequentes
O que é DFM na moldagem por injeção?
DFM in injection molding means designing plastic parts so they can be manufactured efficiently and consistently. It helps reduce defects, tooling changes, cycle time issues, and production cost before tooling begins.
What wall thickness is best for injection molding?
Consistent wall thickness usually performs better than thick sections with large transitions. Balanced walls improve cooling, reduce sink marks, and help maintain dimensional stability during molding.
Why is draft angle important in injection molding?
Draft angles help parts release from the mold without sticking or surface damage. Proper draft reduces ejection force and helps maintain surface quality during production.
What causes sink marks in injection molded parts?
Sink marks usually happen when plastic cools unevenly in thick sections or oversized ribs. Reducing local mass and improving wall consistency helps prevent visible surface depressions.
How do undercuts affect mold cost?
Undercuts often require sliders, Levantadores, or additional tooling mechanisms. These features increase mold complexity, machining time, Manutenção, and production cost.
How do you avoid warping in plastic parts?
Warping is reduced by maintaining uniform wall thickness, balanced cooling, and proper rib placement. Uneven shrinkage is one of the main causes of part distortion.
Compartilhar:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
