



Inspeção de Desgaste do Limite de Molde: Medições e pistas de falha
A proper mold limit pin wear inspection combines visual evidence with controlled dimensional measurements. A polished contact face alone does not prove that the pin is damaged, while a pin that appears clean may still have lost diameter, effective height, or straightness.
The pin should be compared with a controlled drawing, an approved inspection record, a qualified spare, or a documented historical baseline. There is no universal wear allowance or replacement cycle that applies to every mold.
Os pinos de limite são uma parte do sistema mais amplo de substituição Peças padrão para molde (inferido). This guide focuses only on how to inspect their wear, interpret failure clues, and document the next technical action.
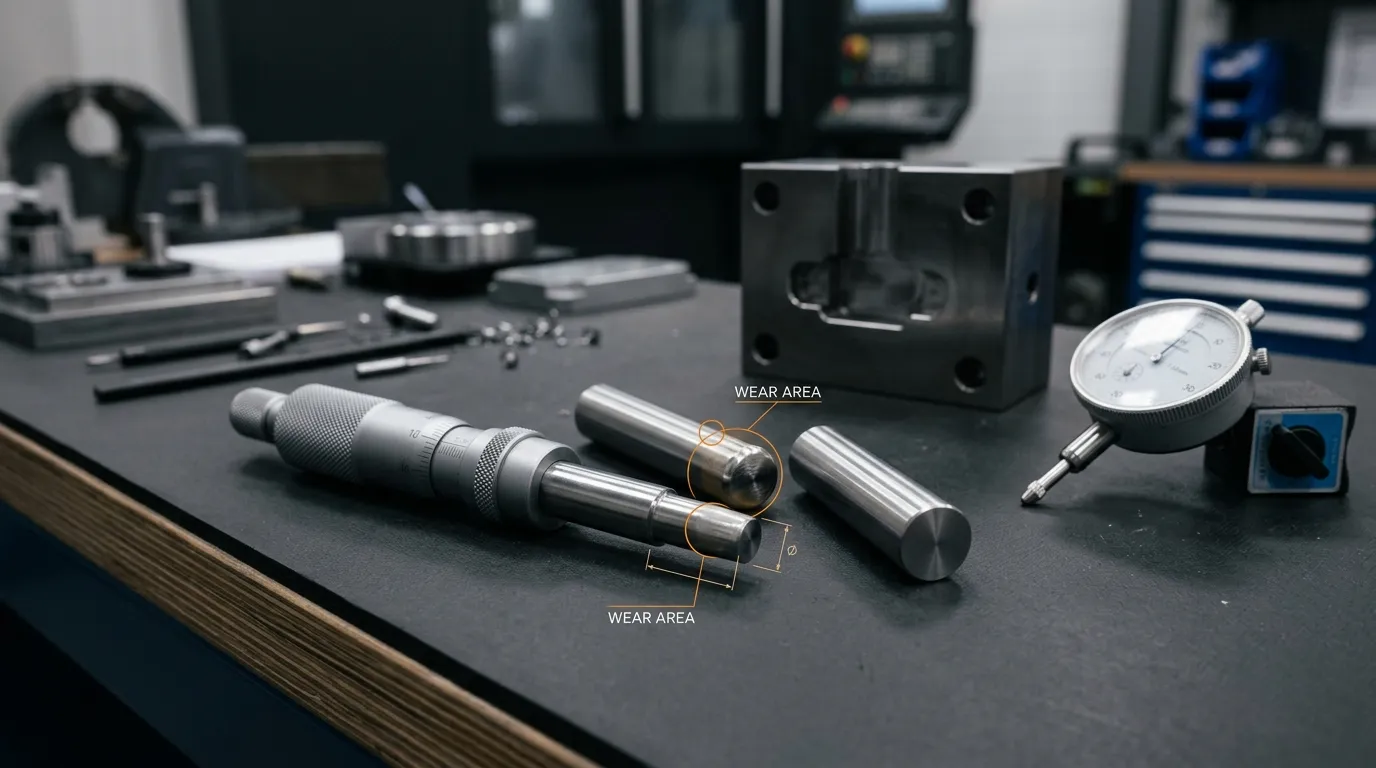
Estabeleça uma Referência de Inspeção Segura e Válida
Before opening, removing, or measuring a limit pin, isolate the molding machine and control all stored energy according to the procedures that apply at the facility. Stored hydraulic pressure, springs, suspended mold sections, gravity, and moving plates can remain hazardous even after the machine has stopped.
Para os locais de trabalho dos EUA, OSHA 29 CFR 1910.147 provides requirements for controlling hazardous energy during servicing and maintenance. Other countries and regions have their own requirements, so the applicable local procedure must control the work.
Before measurement:
- Support the mold and any movable assembly securely.
- Record the pin’s position before removal.
- Photograph visible damage before cleaning it away.
- Remove oil, loose debris, corrosion residue, and dirt from measuring surfaces.
- Check for burrs that could distort the reading.
- Allow the pin and reference equipment to reach a stable measurement condition.
- Confirm which drawing revision or baseline will be used.
Confirm the Pin by Function, Not Name Alone
Os termos Pino limite, pino de parada, e pino de travagem may describe similar travel-limiting functions, but naming is not consistent across mold designs and suppliers.
Identify the component by asking:
- Which plate or assembly does it stop?
- Where is its contact face?
- Which surface does it contact at the end of movement?
- Does it carry stopping load, guide movement, return a plate, eject a part, or locate an assembly?
A return pin, pino ejetor, Guia, dowel, or locating pin should not be assessed using a limit-pin procedure simply because it has a similar cylindrical shape.
Escolha a referência antes de tirar as medições
A measured value has little meaning until it is compared with a valid requirement. Use the strongest available reference in this order:
- Desenho controlado de componentes ou moldes
- Especificação OEM ou padrão de inspeção aprovado
- Relatório de inspeção aprovado anterior
- Reserva nova qualificada
- Medições históricas a partir da mesma posição do pino
- Comparação relativa com pinos correspondentes do mesmo conjunto
Confirm the units, datum surfaces, Tolerâncias, and drawing revision. A nominal length measured from the wrong shoulder or reference face may produce a precise but useless result.
When a result is close to an acceptance limit, measurement uncertainty also matters. ISO 14253-1:2017 addresses how specification limits and measurement uncertainty affect conformity decisions.
Manufacturing tolerances listed on a supplier’s product page should not automatically be treated as service-wear limits. New-part acceptance and continued-service acceptance are different engineering decisions.
Inspecione o pino e seu sistema de contato antes de medir
Begin with a systematic visual examination. Use strong lighting and magnification where needed, but inspect the surrounding components as well as the pin itself.
Check these areas:
- Contato ou parar a face
- Borda externa da face de registro
- Haste cilíndrica
- Transições de diâmetro
- Ombro ou cabeça
- Threads e recursos de retenção
- Superfície de assentos
- Superfície de parada correspondente no molde
- Outros pinos que compartilham a mesma carga de parada
Look for polishing, flattened areas, mushrooming, Pontuação, metal transfer, Pitting, Corrosão, rachaduras, Bordas lascadas, Dano na rosca, and fretting around retained interfaces.
The mating stop surface deserves equal attention. An indentation, Burr, embedded particle, or worn pocket can change the functional stopping position even when the pin itself remains close to its original length.
Separar o polimento normal de testemunhas do dano anormal
A centered and stable polished witness mark may simply show where normal contact occurs. It becomes more concerning when the pattern changes shape, moves toward one edge, or differs significantly between pins in the same set.
| Observação | Interpretação inicial |
|---|---|
| Centered, even polishing | Pode indicar contato normal e equilibrado |
| Marca unilateral ou diagonal | Possible misalignment, unequal height, ou carregamento lateral |
| Face de registro achatada | Impacto repetido ou carga concentrada |
| Borda em cogumelo | Deformação plástica na face de contato |
| Pontuação longitudinal | Abrasive debris, Contato deslizante, or misalignment |
| Metal borrado ou captador | Possível desgaste por galha ou adesivo |
| Rachaduras ou bordas lascadas | Danos estruturais que exigem escalada imediata |
| Ferrugem ou cavidades | Perda de material relacionada à corrosão ou condições ruins de armazenamento |
These observations are clues, not final diagnoses. Desgaste unilateral, por exemplo, may come from a bent pin, unequal pin heights, Desgaste do sistema de guias, a damaged seat, or an uneven mating surface.
Measure Diameter Wear, Taper, and Ovality
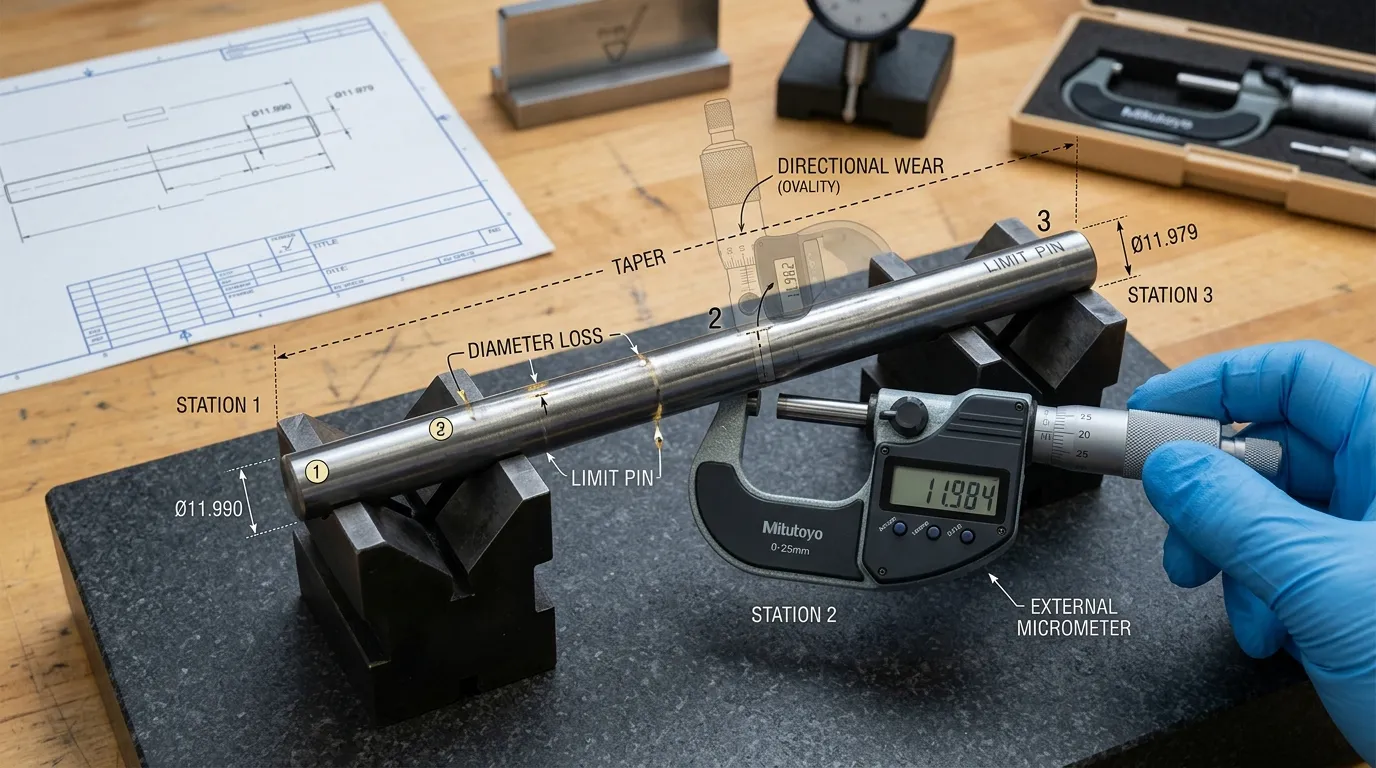
A single diameter reading cannot describe the complete wear condition of a limit pin. Measurements should be taken at repeatable axial locations and in more than one rotational orientation.
An external micrometer is usually more suitable than a caliper when small diameter changes must be evaluated. ISO 3611:2023 defines design and metrological characteristics for external micrometers. Calipers are useful for preliminary checks, but their capability must match the tolerance and expected amount of wear. Their general metrological characteristics are covered by ISO 13385-1:2019.
A practical measurement sequence is:
- Mark the measurement locations along the shank.
- Measure near the upper working area.
- Measure near the centre.
- Measure near the lower working area or seat, where accessible.
- At each location, take readings in at least two rotational orientations.
- Record the position and orientation of every reading.
- Compare the results with the drawing, spare, baseline, and corresponding pins.
This pattern helps separate several conditions:
- Diameter loss: The measured diameter is smaller than the approved reference.
- Taper: Diameter changes progressively along the pin’s length.
- Ovalidade: Readings differ when the pin is rotated at the same axial position.
- Vestimenta local: One short area shows greater loss than the rest of the shank.
Directional diameter loss often supports an investigation into side loading or alignment. Progressive axial wear may indicate contact in a specific working zone rather than uniform material loss.
Do not assign a universal rejection value. The acceptable difference depends on the controlled design, Ajuste, Carregar, and function of the individual mold.
Check Length, Protrusion, and Effective Stop Height
Overall length is not always the most important axial measurement. The functional dimension may be free length, installed protrusion, shoulder-to-face distance, recess depth, or assembled stop height.
First identify the dimension that actually controls plate movement. Then check:
- Comprimento total ou livre
- Deformação face de contato
- Protuberância instalada
- Assentos no ombro
- Engajamento de fios
- Profundidade do assento
- Condição de superfície de acoplamento
- Altura relativa dos pinos correspondentes
A pin may measure correctly after removal but still sit too low because of debris under the shoulder, Dano na rosca, seat wear, or an incorrect replacement geometry. The opposite can also occur: the pin may appear shortened when the real loss is an indentation in the opposing stop surface.
Use a height gauge, depth micrometer, height micrometer, or another suitable setup based on the controlled datum and accessibility. The setup must be rigid enough to produce repeatable results.
Compare todos os pinos que compartilham a carga de parada
Several limit pins may work together to stop the same moving plate. Their effective heights should be compared because one high pin can contact first and carry more load than the others.
Verifique se:
- Contact patterns appear on all corresponding pins.
- Protrusion or effective height is consistent.
- One pin has a larger polished or deformed area.
- One position shows deeper indentation on the mating surface.
- A previously replaced pin differs from the remaining set.
- One pin contacts before the plate becomes parallel.
Replacing only the visibly damaged pin may not solve the problem if the set has unequal heights or if another component caused the load imbalance.
Check Runout, Dobra, and Straightness
A pin subjected to side loading, collision, or severe misalignment may bend without showing major diameter loss.
Where the geometry permits, support the clean pin on suitable datum surfaces or V-blocks and use a dial indicator to measure variation during rotation. Record the indicator position and support arrangement so the test can be repeated.
Before accepting the result, Verifique para:
- Rebarbas sob os pontos de suporte
- Sujeira nos blocos em V
- Superfícies cilíndricas danificadas
- Ombros irregulares
- Má alinhamento dos indicadores
- Força de medição excessiva
- Movimento do suporte
Runout, Retidão, and coaxiality are related but not interchangeable terms. ISO 1101:2017 provides the geometrical tolerancing framework for form, Orientação, Localização, e runout. Straightness terminology is further defined in ISO 12780-1:2011.
The total indicated variation from a workshop setup should not automatically be treated as the drawing’s straightness error. It is an inspection result that must be interpreted against the specified geometry and measurement method.
When bending or directional wear is found, inspect the mold’s alignment system. Desgastado mold pins and bushings can allow plate movement that places abnormal side load on a limit pin.
Interprete os padrões de desgaste sem ir direto à causa raiz
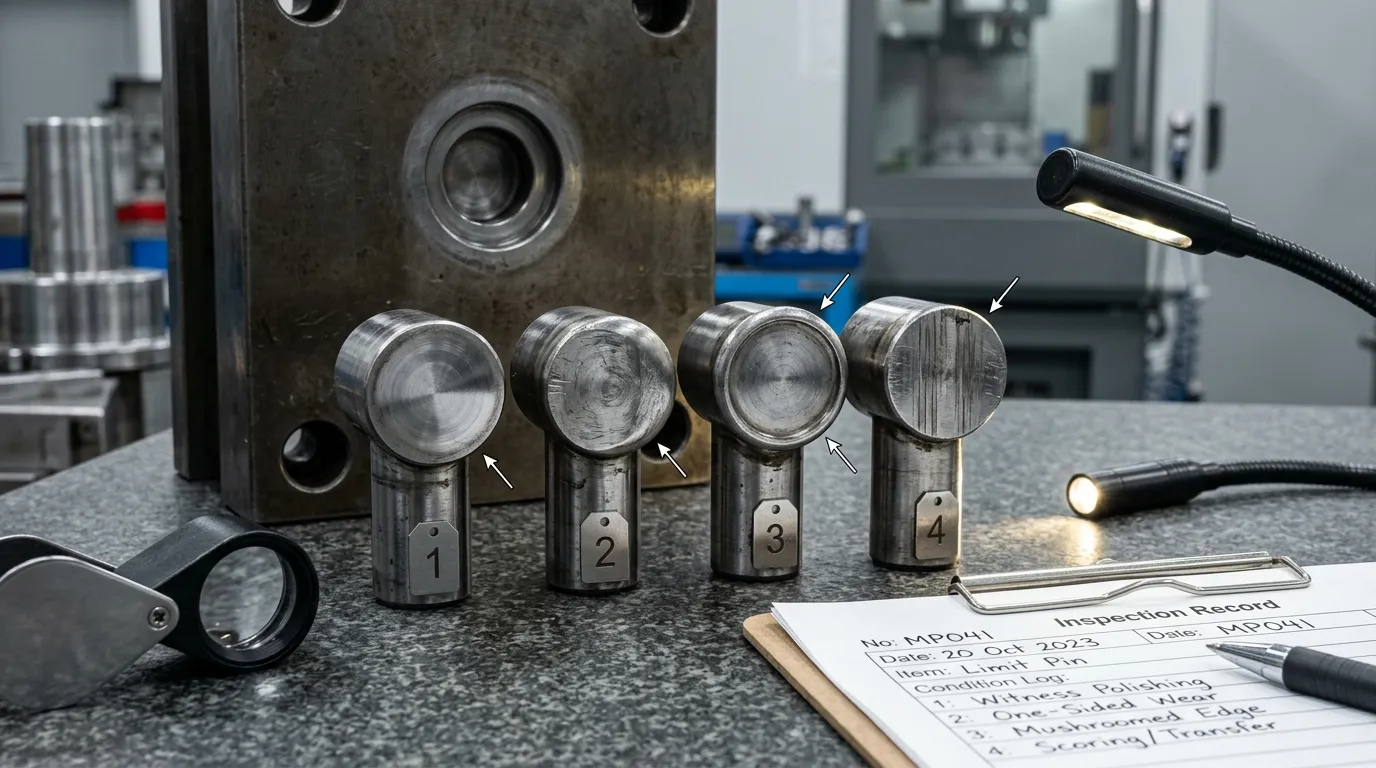
Use each wear pattern to guide further inspection rather than treating it as proof.
| Pista de falha | Possíveis causas | Verificações de confirmação | Resposta imediata |
| Marca de testemunha unilateral | Desalinhamento, unequal pin height, angled mating surface | Compare matched-pin heights, guide condition, plate parallelism | Continue o diagnóstico antes de trocar o pino |
| Rosto achatado ou em forma de cogumelo | Impacto repetido, overtravel, insufficient contact area, unequal loading | Check effective height, stroke, mating surface, other pins | Meça a perda axial e aumente se a deformação estiver ativa |
| Pontuação longitudinal | Debris, desgaste abrasivo, Contato deslizante, Alinhamento ruim | Inspect bore or surrounding surface, Contaminação, Sistema de guias | Remover a contaminação e avaliar a perda de diâmetro |
| Galling ou transferência de metal | Alta fricção, Desgaste adesivo, poor surface compatibility | Look for transferred material, heat discoloration, rough mating surface | Parar danos contínuos e investigar o par de contato |
| Local diameter loss | Desgaste por contato concentrado ou abrasivo | Diâmetro do mapa em várias posições axiais | Compare com desenhos e dados históricos |
| Afunilamento ou ovalidade | Directional wear, side load, uneven support | Rotate measurements, inspect alignment and seating | Determine se o desgaste está estável ou está progressivo |
| Corrida excessiva | Dobra, collision, Carregamento lateral | Repeat indicator setup, inspect guide system and plate movement | Revisão de engenharia antes do reuso |
| Cavidades ou corrosão | Umidade, Exposição química, poor storage | Examine componentes próximos e condições de armazenamento | Avaliar profundidade e efeito estrutural |
| Rachaduras ou bordas lascadas | Impact fatigue, sobrecarga, material damage | Inspecionar com ampliação adequada ou método NDT aprovado | Retirar do serviço e escalar |
| Dano na linha ou ombro | Loosening, improper seating, repeated movement | Check seat, Engajamento, retention and installed height | Corrija o problema de retenção antes de substituir |
Abnormal sound, Fixação, plate travel changes, Flash, or mismatch can justify an unscheduled inspection. They do not independently prove that the limit pin is the failed component.
Decide Whether to Continue, Monitor, Substituir, or Escalate
The final decision should combine dimensional results, visible condition, functional evidence, and the approved acceptance criteria.
| Decisão | Condição apropriada |
| Continuar em serviço | Measurements meet approved criteria, contact is stable, no structural damage is present, and associated components are acceptable |
| Monitor | Minor measurable change is permitted, the condition is stable, and a documented reinspection plan is approved |
| Substituir | The pin is outside its controlled specification, has unacceptable height variation, Deformação severa, damaged retention features, rachaduras, Lascamento, or active galling |
| Revisão de engenharia | No valid specification exists, results conflict, uncertainty is too high, damage keeps returning, or system-level misalignment is suspected |
A pin should not be polished or reground automatically. Material removal can change its effective length, stop height, contact timing, e distribuição de carga. Serviceability depends on the component’s function and approved dimensional limits.
Generic cycle-count recommendations are also unreliable. Two molds using similar pins may create very different impact loads, alignment conditions, contamination exposure, and maintenance histories.
Registre a inspeção e evite erros comuns de medição
A useful inspection record should include:
- Identificação de mofo
- Posição do pino
- Número do desenho e revisão
- Referência utilizada
- Instrumento de medição e resolução
- Locais de medição
- Valores e unidades registrados
- Fotografias
- Condição de superfície de acoplamento
- Condição dos pinos correspondentes
- Sintomas operacionais relevantes
- Destino final
- Gatilho de reinspeção ou intervalo aprovado
Consistent records make it possible to see whether wear is stable or accelerating.
Common errors include:
- Measuring through oil, Tranquilidade, dirt, or burrs
- Medindo um componente quente com dados de referência à temperatura ambiente
- Fazendo apenas uma leitura de diâmetro
- Mudança de locais de medição entre inspeções
- Usar um calibre quando é necessária maior resolução
- Confusão do runout indicado com a retidão definida pelo desenho
- Ignorando o assento ou a superfície de parada
- Comparando pinos que não são funcionalmente correspondidos
- Remoção de danos antes de fotografar
- Tratar as tolerâncias de fabricação de peças novas como limites de desgaste em serviço
Broader tolerance, aço, and inspection considerations for Peças de molde de precisão can support replacement planning, but the used pin must still be judged against its own controlled requirements.
Prepare os dados necessários para um pino substituto ou personalizado
When inspection confirms that a replacement is required, prepare enough information to reproduce the functional geometry rather than sending only the worn component’s current dimensions.
Fornecer:
- Desenho controlado ou esboço dimensionado
- Dimensões nominais
- Medidas de desgaste
- Altura funcional do batente
- Geometria de face de contato
- Ombro, cabeça, Tópico, and seat details
- Material and hardness requirement, where known
- Quantidade
- Requisitos de conjuntos pareados
- Fotografias do pino e da superfície de acoplamento
- Resultados da inspeção
- Causa provável da falha
- Documentação de inspeção obrigatória
O SunshinePro lista padrão e não padrão pino de limite de molde options, including customization from dimensional requirements. Its published product information identifies S45C/45# steel, Esmerilamento de precisão, threaded construction, Tratamento térmico a vácuo, and a stated hardness of 15–17 HRC for that listed product.
Those details are product-specific. They should not be assumed to apply to every existing pin or used as universal replacement criteria.
Replacing the pin without correcting damaged seating, an indented stop surface, unequal matched heights, or alignment problems can cause the new component to fail in the same way. After the cause and required geometry are documented, the drawing, measurements, and photographs can be submitted through SunshinePro’s Página de contato for a standard or custom replacement discussion.
Compartilhe:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
