



D2 vs M2 Aço para pinos de perfuração: Wear, Resistência, e Velocidade
For punch pins, D2 and M2 solve different combinations of wear, Impacto, and thermal stress. D2 is often a practical choice when gradual abrasive wear is the main concern and the die operates under controlled cold-work conditions. M2 may be the stronger candidate when the punch faces repeated edge chipping, difficult stock, long production runs, slender geometry, or sustained heat at the cutting edge.
Neither material is automatically better. Press speed alone does not determine the answer, and a harder punch is not always a more durable punch. Liberação, Tratamento térmico, Geometria, Alinhamento, Lubrificação, and the actual failure pattern can matter as much as the steel grade.
Material selection is also only one part of a complete die system. The broader relationship between punches, isso, Autorização, and tooling requirements is covered in SunshinePro’s Guia de matrizes de punção (inferido).
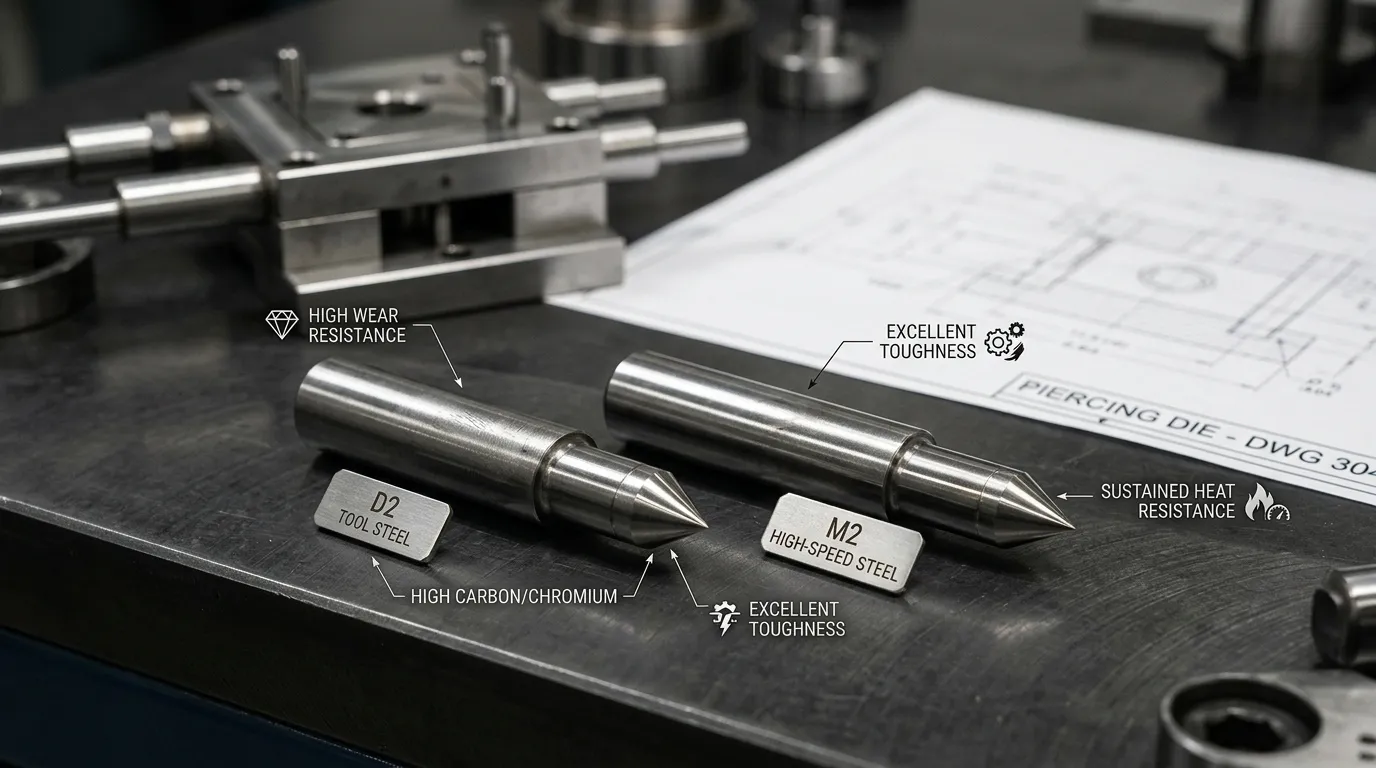
Comparação do pino de perfuração D2 vs M2 em um olhar
| Fator de comparação | Aço para ferramentas D2 | Aço de alta velocidade M2 |
|---|---|---|
| Família do aço | Aço para ferramentas de trabalho a frio | Aço de alta velocidade |
| Força típica de seleção | Forte resistência ao desgaste sob condições controladas de trabalho a frio | Balanced wear resistance, Estabilidade de borda, Resistência, and hot hardness |
| Limitação principal | Can become vulnerable to chipping or fatigue when the hardness, Geometria, or loading is too aggressive | Custos mais altos de material e processamento podem não ser justificados em aplicações leves |
| Desgaste abrasivo | Frequentemente um candidato forte onde o desgaste abrasivo gradual predomina | Also wear resistant, especially where wear occurs with heat or repeated impact |
| Resistência e lascamento | Dependente da aplicação; geometry and heat treatment must be controlled | Frequentemente considerado quando D2 sofre lascamento recorrente na borda em condições estáveis |
| Calor sustentado | Menos adequado para aplicações onde a aresta de corte permanece quente por longos períodos | Mais conhecido por manter a dureza sob temperaturas elevadas de serviço |
| Condições de melhor ajuste | Stable alignment, suitable clearance, controlled impact, moderate thermal demand | Long runs, difficult stock, higher thermal demand, socos esguios, or expensive downtime |
| Direção de custos | Comumente considerado o ponto de partida mais econômico | Geralmente avaliado quando a confiabilidade melhorada pode compensar o custo adicional |
| Verificação obrigatória | Grau exato, Tratamento térmico, Dureza, Geometria, e condições de produção | Grau exato, Tratamento térmico, condição de têmpera, Dureza, e condições de produção |
These are selection tendencies, not guaranteed performance rankings. A poorly supported M2 punch can fail before a correctly designed D2 punch, while an over-hardened or misaligned D2 punch can chip before its wear resistance becomes useful.
Por que D2 e M2 se comportam de forma diferente em um soco
D2 is a high-carbon, high-chromium cold-work tool steel. It is commonly associated with wear resistance, compressive-load capability, and dimensional stability in tools operating without sustained high-temperature exposure. O Folha técnica do BÖHLER K110, which covers a D2-family grade, lists punching and stamping tools among its applications.
M2 belongs to the molybdenum high-speed-steel family. Its alloy system is designed to retain hardness and cutting performance under greater thermal demand. O Ficha técnica do BÖHLER S600, covering an M2-family grade, emphasizes wear resistance, Resistência, Estabilidade de borda, Resistência à compressão, and red hardness.
The difference cannot be reduced to a single Rockwell hardness value. Two punch pins at a similar HRC may still behave differently because of:
- Composição da liga e distribuição do carboneto
- Austenitização, Têmpera, and tempering conditions
- Microestrutura mantida
- Condição da superfície de moagem e EDM
- Geometria do punção e suporte
- Temperatura durante a produção
- O tipo de desgaste ou fratura ocorrendo
The agreed material standard therefore matters. ASTM A681 covers alloy tool steels such as D2, enquanto ASTM A600 covers high-speed tool steels such as M2.
Nomes de Grau que os Compradores Não Devem Considerar Equivalentes Automáticos
Worldwide sourcing often involves several designation systems. D2 may be discussed alongside SKD11 or 1.2379, while M2 may be cross-referenced with SKH51, SKH9, or 1.3343.
These names should not be accepted as interchangeable without checking the applicable standard, Química, production route, and final heat-treated condition. The drawing or purchase specification should identify the agreed grade rather than relying on a general trade name.
DC53 also should not be described as another name for standard D2. It is a separate modified cold-work steel with its own processing and performance characteristics.
Resistência ao desgaste: Identify the Wear Mechanism Before Choosing
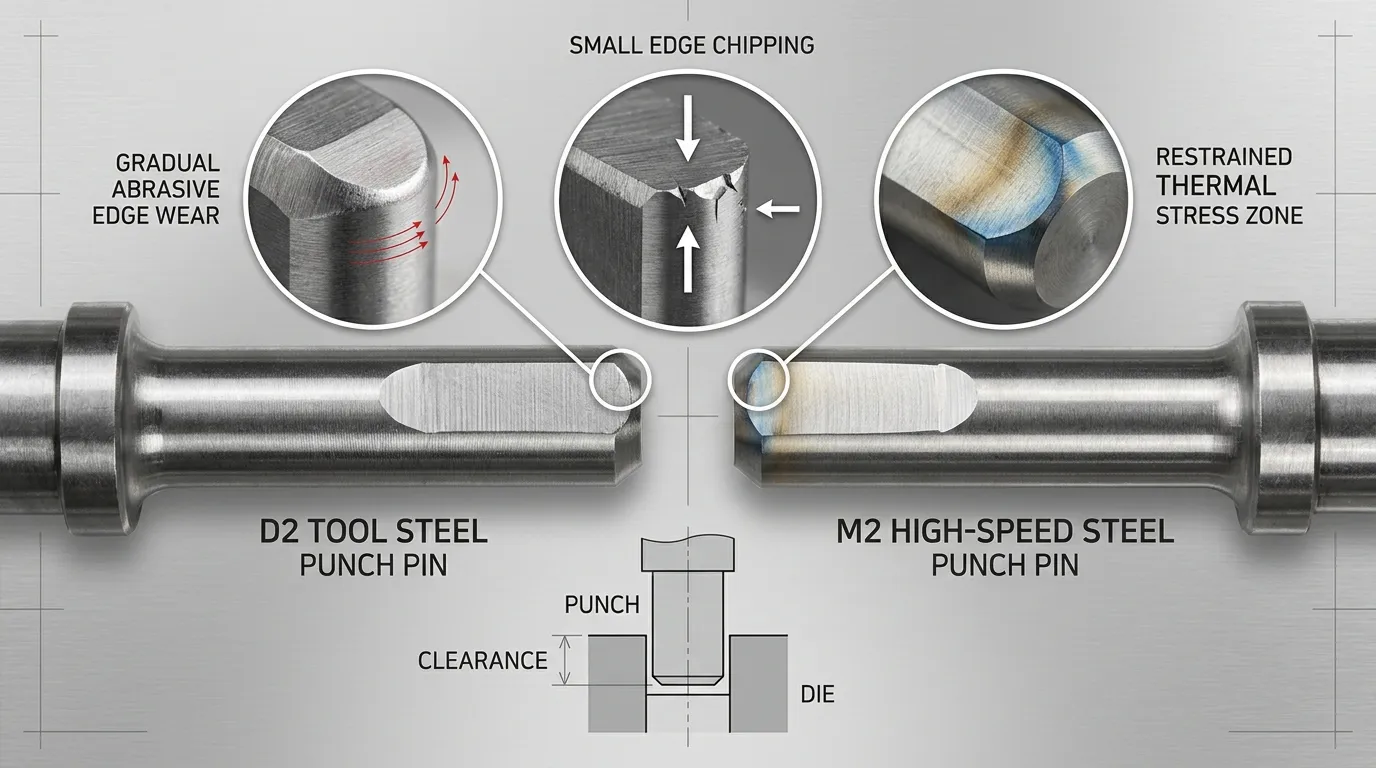
Asking which steel has “better wear resistance” is incomplete until the wear mechanism is known.
Desgaste abrasivo gradually removes material from the punch edge or flank. It may be driven by hard particles, escala, an abrasive workpiece, or repeated sliding contact. D2 is often considered when this predictable, gradual wear is the primary problem and shock loading remains controlled.
Desgaste adesivo e galhas involve material transfer, captador, or local seizure between the punch and workpiece. These problems are influenced heavily by workpiece material, Acabamento superficial, Lubrificação, Autorização, e revestimento. Changing from D2 to M2 may not correct galling if friction and material adhesion remain the real causes.
Desgaste combinado com lascamento ou calor creates a different selection problem. M2 may provide a more useful performance balance where the edge must resist abrasion while also tolerating repeated stress and sustained temperature.
Before changing steel, inspect how the existing punch is deteriorating:
| Condição observada | Provável que é um problema a investigar | Implicação material |
| Smooth, gradual edge recession | Desgaste abrasivo | D2 may remain suitable; compare maintenance interval and total cost |
| Recolha de material ou depósitos ásperos | Irritação, Fim, Lubrificação, Revestimento | Corra as condições da superfície antes de culpar o aço a granel |
| Pequenos pedaços se rompendo da borda | Lascamento, Dureza excessiva, Geometria, Autorização, Carregamento lateral | M2 pode ser considerado após o controle das causas do sistema |
| Desgaste rápido durante longas corridas ininterruptas | Combinação de abrasão e calor | A capacidade de resistência a quente do M2 pode se tornar mais relevante |
SunshinePro’s die punch pin page lists precision grinding and TiN and TiCN coating options. These processes can support surface condition and wear control, but a coating cannot compensate for unsuitable steel, Alinhamento ruim, incorrect clearance, or weak punch support.
Resistência, Lascamento, and Punch Geometry
Punch toughness is not determined by the steel name alone. The final hardness, Tratamento térmico, edge shape, Comprimento sem suporte, and loading direction all affect whether the punch bends, chips, or develops fatigue cracks.
A large, well-supported round punch and a long, narrow punch do not place the same demands on the material. Small-diameter punches, sharp internal features, narrow points, and long unsupported sections create greater stress concentration and bending risk.
Repeated chipping can result from:
- Dureza excessiva para a geometria
- Folga incorreta entre punção e matriz
- Má orientação ou alinhamento
- Carregamento lateral
- Suporte insuficiente da cabeça ou do corpo
- Dano de moagem
- Uma camada de recast descontrolada de EDM
- Defeitos no tratamento térmico
- Sobrecarga local devido à variação de estoque
A published failure analysis of an AISI D2 punch found that punch damage could involve fatigue, carbide cracking, excessive loading, heat-treatment issues, backup-plate wear, Autorização, and guiding conditions. The study reinforces a basic rule: changing the material without correcting the mechanical cause may only move the failure to another location. Veja o estudo em fadiga e desgaste em um soco AISI D2.
M2 may deserve evaluation when a D2 punch repeatedly chips despite correct alignment, suitable clearance, stable heat treatment, and adequate support. It should not be treated as a substitute for investigating the die system. A more complete diagnosis of side loading, Autorização, Guiamento, and fracture causes belongs in the guide to Quebra de punção em matrizes de estampagem.
Quando a velocidade de pressão torna a dureza quente do M2 relevante
The term “high-speed steel” often leads to an oversimplified rule: fast press equals M2. Actual punch conditions are more complicated.
Strokes per minute affect the number of loading events, but they do not directly state the cutting-edge temperature. Thermal demand also depends on:
- Duração contínua
- Resistência e espessura da peça
- Tamanho do furo e geometria do perfurador
- Folga para o punção
- Atrito e galha
- Lubrificação
- Dissipação de calor entre os golpes
- A duração e a frequência das paragens de produção
A fast press running short batches of thin, manageable stock may produce less sustained edge heat than a slower press running thick, high-strength material continuously.
M2’s hot hardness becomes more valuable when the cutting edge remains hot enough for ordinary cold-work performance to deteriorate. That condition may appear during long progressive-die runs, difficult stock punching, Alta fricção, or inadequate cooling between cycles.
D2 can still be suitable at a high numerical press speed when thermal load, Impacto, and chipping risk remain controlled. M2 should therefore be selected because of the complete duty cycle, not because the press specification contains a high strokes-per-minute number.
D2 or M2? Choose by Failure Mode and Application
The following table provides a starting direction. It is not a substitute for examining the die, Peça de trabalho, Tratamento térmico, and failed punch.
| Condição de aplicação | Provável candidato titular | Motivo | Verifique antes de decidir |
| Estábulo, gradual abrasive wear | D2 | Uma forte capacidade de desgaste a frio pode ser suficiente | Dureza, Intervalo de afiação, stock abrasiveness |
| A aresta D2 faz lascas repetidamente | O M2 pode ser avaliado | Um equilíbrio mais amplo entre tenacidade e estabilidade entre aresta pode ajudar | Liberação, Alinhamento, Geometria, Tratamento térmico |
| Produção longa e ininterrupta com calor sustentado nas bordas | M2 | A dureza quente se torna mais relevante | Actual temperature drivers, Atrito, Lubrificação |
| Punção de pequeno diâmetro ou esguia | O M2 pode ser avaliado | A geometria pode exigir maior resistência a lascamento e fadiga | Comprimento sem suporte, Guiamento, Suporte de cabeça |
| Punção de volume moderado em aço suave ou carbono-carbono | D2 pode ser suficiente | A demanda térmica e de impacto pode não justificar M2 | Stock thickness, Autorização, desired maintenance interval |
| Material inoxidável ou propenso a galhas | Dependente da aplicação | Atrito, Aderência, and heat may dominate | Lubrificação, Acabamento superficial, Revestimento, Autorização |
| Folha grossa ou de maior resistência | M2 pode oferecer uma vantagem | Cargas mais altas podem aumentar a tensão nas bordas e o calor | Diâmetro do punção, press force, Apoio, hole geometry |
| O tempo de inatividade é substancialmente mais caro do que o custo da ferramenta | M2 pode ser economicamente justificado | O custo inicial adicional pode ser aceitável se a confiabilidade melhorar | Registros de produção e resultados de ensaios controlados |
Condições típicas onde D2 pode ser suficiente
D2 remains a reasonable candidate when the punch experiences predictable wear under stable cold-working conditions. Suitable clearance, strong guidance, adequate support, and controlled hardness allow its wear resistance to be used without excessive chipping.
It can be a practical choice for moderate production duties where current sharpening intervals are acceptable and the application does not create sustained heat or severe impact.
Condições em que o M2 pode justificar seu custo mais alto
M2 becomes more attractive when a punch must maintain its edge under combined wear, repeated stress, and thermal demand. Examples include long production runs, difficult or higher-strength stock, slender punch geometry, and applications where recurring D2 chipping continues after system problems have been corrected.
The economic case is strongest when unplanned breakage or press downtime costs much more than the difference in punch material and processing.
Steel Grade Alone Will Not Fix Clearance, Alinhamento, or Heat-Treatment Problems
Before replacing D2 with M2, confirm that the current punch is being tested fairly. No mínimo, Análise:
- Folga para o punção
- Concentricidade e alinhamento do punção
- Condição do guiador e do bucha
- Suporte de punção e comprimento não suportado
- Variação de espessura e dureza da peça
- Consistência da lubrificação
- Queimaduras por desgaste ou danos nas bordas
- Condição da superfície da EDM
- Dureza final e condição de têmpera
- Condição do revestimento
- Padrão de desgaste na abertura do punção e matriz
Incorrect clearance can increase cutting load, Formação de rebarbas, edge stress, e lascamento. Misalignment can place bending loads on a punch designed mainly for compression. Grinding or EDM damage can also provide a starting point for fatigue cracks.
A punch works as part of a larger assembly. The relationship between the punch, Retinedor, Guias, Buchas, die insert, and support components is covered more broadly in the Guia de componentes do die.
Compare Cost by Downtime and Maintenance, Not Steel Price Alone
D2 may have a lower initial cost in many sourcing situations, but purchase price does not show the complete economic result. M2 may cost more to purchase, Máquina, heat-treat, or grind, yet still be worthwhile if it reduces expensive production interruptions.
A useful comparison should include:
| Fator de custo | Pergunta a avaliar |
| Custo inicial do punção | What is the delivered cost in the specified grade and condition? |
| Afiamento | How many hits occur between scheduled sharpening events? |
| Quebra não planejada | Does the punch wear predictably or fail without warning? |
| Tempo livre | How much production is lost during replacement and die adjustment? |
| Sucata | Does edge deterioration affect burrs, Dimensões, or part quality? |
| Inventário | How many spare punches are required to protect production? |
| Mão de obra de manutenção | How much toolroom time is spent inspecting, Afiamento, and replacing punches? |
M2 is not automatically the lower-cost choice. It becomes economically attractive only when its performance under the actual application reduces enough maintenance, failure, sucata, or downtime to offset the added cost.
O que especificar antes de solicitar um pino perfurador D2 ou M2
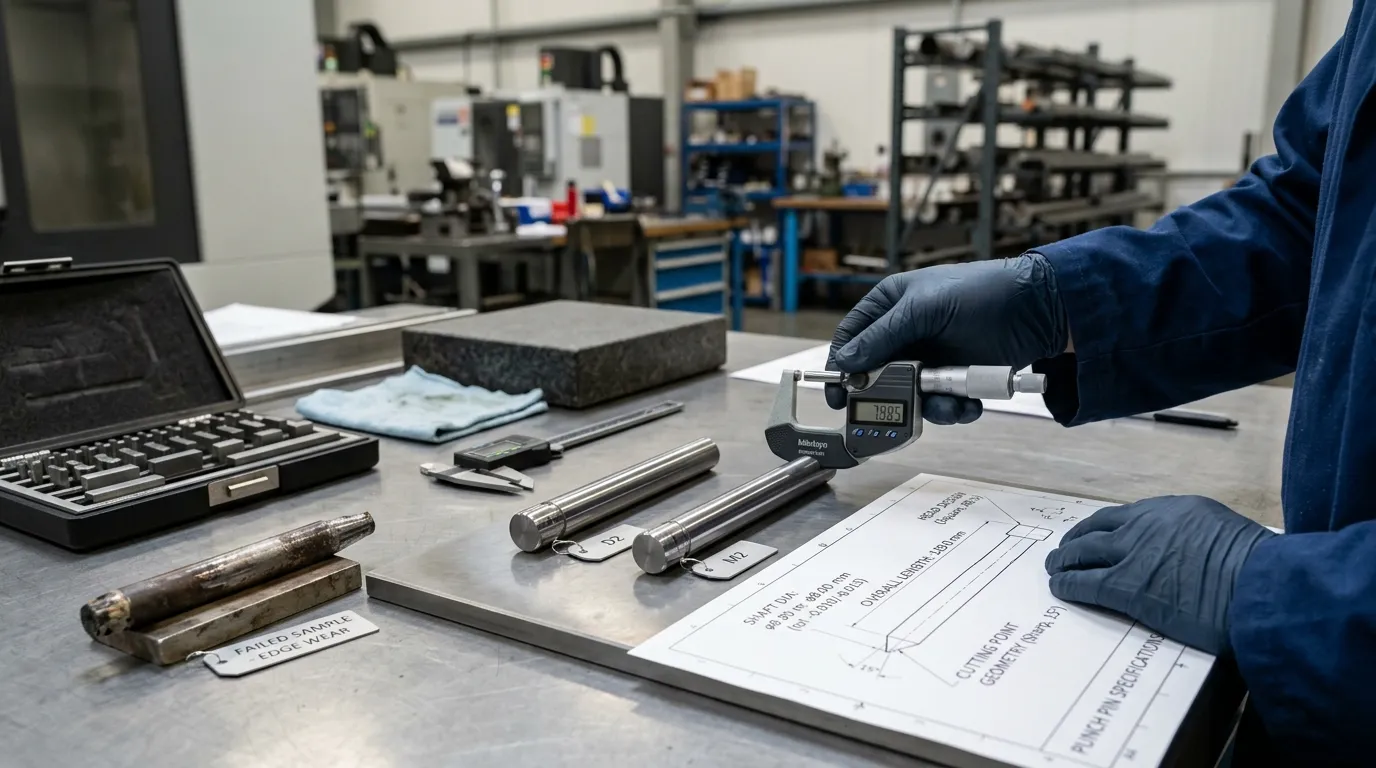
A supplier cannot make a reliable material recommendation from the punch diameter alone. The RFQ should describe both the component and its operating conditions.
Fornecer:
- Um desenho dimensionado
- Diâmetro do punção, Comprimento, and unsupported length
- Projeto do cabeçote e arranjo de suporte
- Point shape, corner radii, and special cutting features
- Material e grau da peça
- Espessura da folha
- Dimensões e formato do furo
- Folga para o punção
- Tipo de prensa e velocidade de operação
- Duração contínua
- Contagem anual esperada de visitas
- Lubrificante e método de aplicação
- Material existente do punção e dureza medida
- Current failure symptom: Desgaste, Galling, Lascamento, Dobra, ou fadiga
- Fotografias ou amostras falhadas quando disponíveis
- Revestimento necessário
- Designação de material acordada e padrão
- Certificado de material exigido
- Documentação de tratamento térmico
- Requisito de inspeção de dureza
- Critérios de aceitação para um teste de produção
SunshinePro states that non-standard components can be produced from customer drawings. É Página do produto do pino Die Punch lists custom diameter, Comprimento, Design da cabeça, Material, e opções de revestimento, together with SKH51, SKH9, DC53, Notas ASP, e carboneto. The page also mentions CNC machining, Esmerilamento de precisão, EDM, e tratamento térmico a vácuo.
That information does not confirm AISI D2 availability. Buyers requiring D2 should ask the supplier to confirm the exact material designation, applicable standard, condição de tratamento térmico, and documentation before ordering.
A controlled trial remains the most reliable final check. Compare D2 and M2 using the same drawing, Autorização, Imprensa, workpiece batch, lubrificante, Estado do revestimento, e método de inspeção. Record the hit count and actual failure mechanism rather than judging only by whether the punch still appears usable.
Quando nem D2 Convencional nem M2 são a resposta correta
If both materials fail after clearance, Apoio, Alinhamento, Lubrificação, Geometria, and heat treatment have been corrected, the application may require a different solution.
Possible next steps include reviewing:
- Aço de alta velocidade para metalurgia em pó
- Carbeto
- Um sistema de revestimento diferente
- Geometria revisada do punção
- Guia ou suporte aprimorados
- Alterações na folga ou lubrificação
SunshinePro lists ASP grades and carbide among its punch-pin material categories, but these alternatives should be evaluated against the same application data rather than treated as automatic upgrades.
For a material review or quotation, submit the punch drawing, Detalhes da peça, Condições de produção, and current failure evidence through the Página de contato SunshinePro. The strongest recommendation will come from matching the steel, Tratamento térmico, Geometria, and die conditions to the failure mode the punch must actually survive.
Compartilhe:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
