



Resistência ao desgaste em componentes de molde: Materiais, Revestimentos, and Heat Treatment
Wear resistance in mold components depends on choosing the right steel, revestimento, and heat treatment for the molding environment. Abrasive plastics, sliding contact, and high production cycles can quickly damage cores, Cavidades, and ejector systems. Hardened tool steels, Nitruração, and wear-resistant coatings help reduce maintenance, improve dimensional stability, and extend mold life when matched correctly to the application.
Mold wear is one of the biggest reasons injection molds lose accuracy over time. Gates begin to flash, sliders start galling, and polished surfaces lose consistency. Many of these failures are preventable with better material selection and surface engineering. This guide explains how wear develops in mold components, which materials perform best, and how coatings and heat treatment affect long-term tooling performance.
What causes wear in mold components?
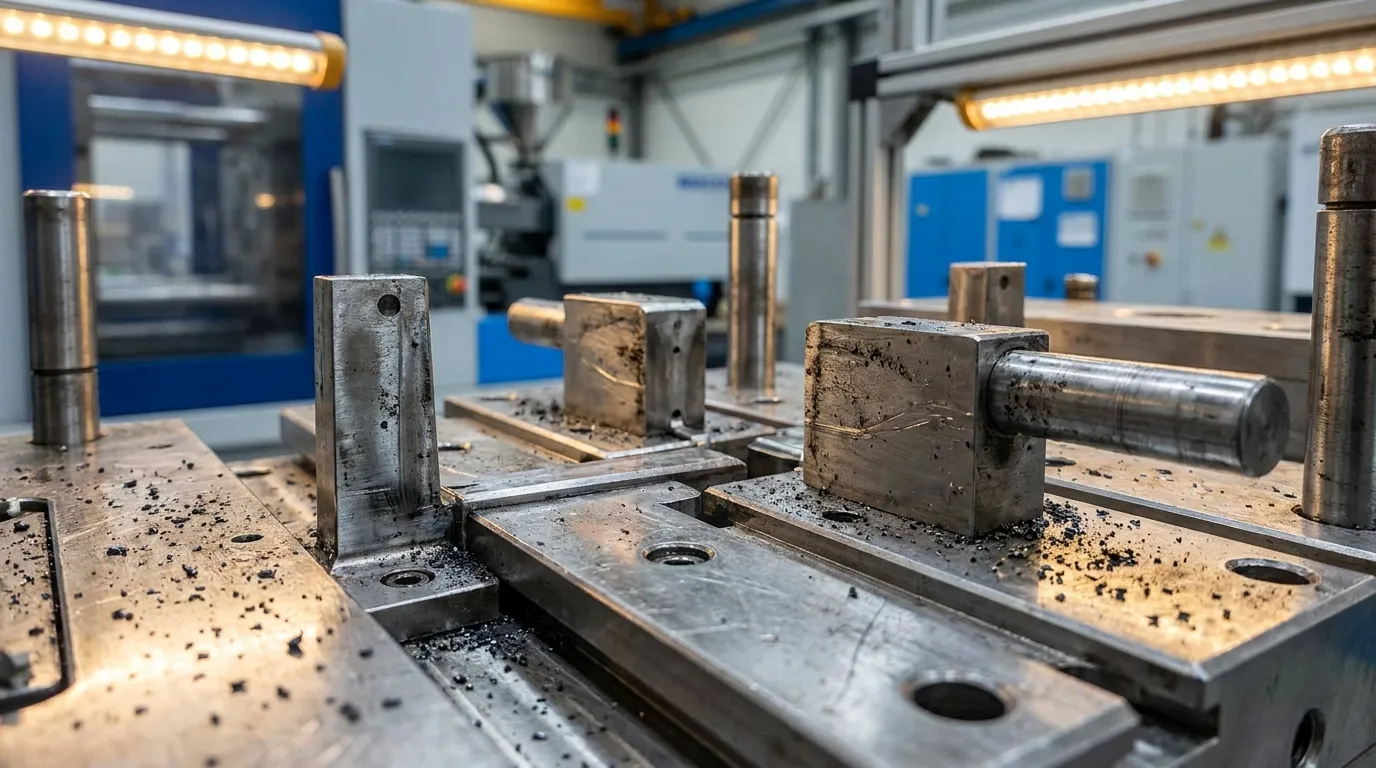
Wear resistance in mold components depends on controlling abrasion, Atrito, and surface fatigue. Resinas preenchidas com vidro, Lubrificação ruim, and repeated cycling accelerate wear on cores, Cavidades, ejector pins, and sliding components.
Most mold wear comes from repeated friction between steel surfaces and abrasive plastic flow. Filled engineering plastics are especially damaging because glass fibers and mineral additives scrape the mold surface during every injection cycle. Com o tempo, this removes material from gates, cores, and shutoff surfaces.
De acordo com pesquisas resumidas por ScienceDirect, wear resistance is affected by hardness, Força, surface roughness, and material structure. In mold tooling, those properties work together rather than independently.
Desgaste abrasivo vs adesivo em moldes
Abrasive wear happens when hard particles cut into the mold surface. This is common with glass-filled nylon, flame-retardant compounds, and mineral-filled resins. Gate inserts and runner transitions usually show the first signs of damage.
Adhesive wear happens when two metal surfaces rub against each other under pressure. Slides, lifters, and ejector systems are common failure points. If lubrication is poor, the surfaces may begin galling, which creates scratches, drag marks, and dimensional drift.
| Tipo de desgaste | Causa Comum | Áreas Típicas de Mofo |
|---|---|---|
| Desgaste abrasivo | Resinas preenchidas com vidro | Portões, Cavidades, cores |
| Desgaste adesivo | Contato metálico deslizante | Slides, lifters, ejectors |
| Fadiga superficial | Ciclismo repetido | Shutoffs, moving inserts |
| Desgaste corrosivo | Aditivos agressivos | Vent areas, Cavidades |
Is hardness the same as wear resistance?
Hardness improves resistance to indentation, but wear resistance depends on toughness, Condição da superfície, Lubrificação, and coating performance. Extremely hard mold steels can still fail if brittleness increases.
Hardness and wear resistance are closely related, but they are not identical properties. A harder steel usually resists scratching and abrasive damage better than a softer steel. Still, extremely high hardness can reduce toughness and increase cracking risk under impact or cyclic stress.
Pesquisa discutida por SilcoTek explains that wear performance depends on the entire surface system. Material structure, friction conditions, coatings, and operating loads all affect long-term durability.
This matters in mold manufacturing because the hardest steel is not always the safest choice. A high-impact mold with moving slides may perform better with slightly lower hardness and better toughness. That tradeoff often reduces unexpected downtime and expensive repairs.
For molds that require advanced thermal processing, a detailed overview of Tratamento térmico com mofo can help clarify how hardness targets affect mold performance.
| Propriedade | O que Ele Melhora | Risco Potencial |
|---|---|---|
| Alta dureza | Resistência à abrasão | Fragilidade |
| Alta resistência | Resistência a trincas | Desgaste mais rápido |
| Revestimento superficial | Redução do atrito | Falha do revestimento se o substrato for fraco |
Which mold components experience the most wear?
Gate areas, ejector pins, slides, and core features typically wear fastest because they experience concentrated friction, Pressão, and repeated resin flow. Abrasive fillers like glass fiber increase damage significantly.
Not every mold component wears at the same rate. High-contact and high-flow areas usually fail first, especially in molds running abrasive engineering plastics. Concentrated pressure and repeated motion accelerate material loss over time.
The following components typically require the highest wear resistance:
- Inserts de gate expostos a fluxo rápido de resina
- Pinos ejetores com movimento deslizante repetitivo
- Pinos de núcleo que lidam com geometria de parede fina
- Ferrolhos e levantadores sob pressão lateral
- Cavidades moldando materiais preenchidos com vidro
A mold producing glass-filled nylon electrical connectors may show gate wear after only 250,000 cycles if the tooling steel is untreated. Em muitos casos, nitrided H13 steel lasts significantly longer than untreated H13 under the same production conditions.
For a broader overview of mold architecture and tooling functions, o Guia de componentes do molde explains how these parts interact during injection molding cycles.
Which mold steels offer the best wear resistance?
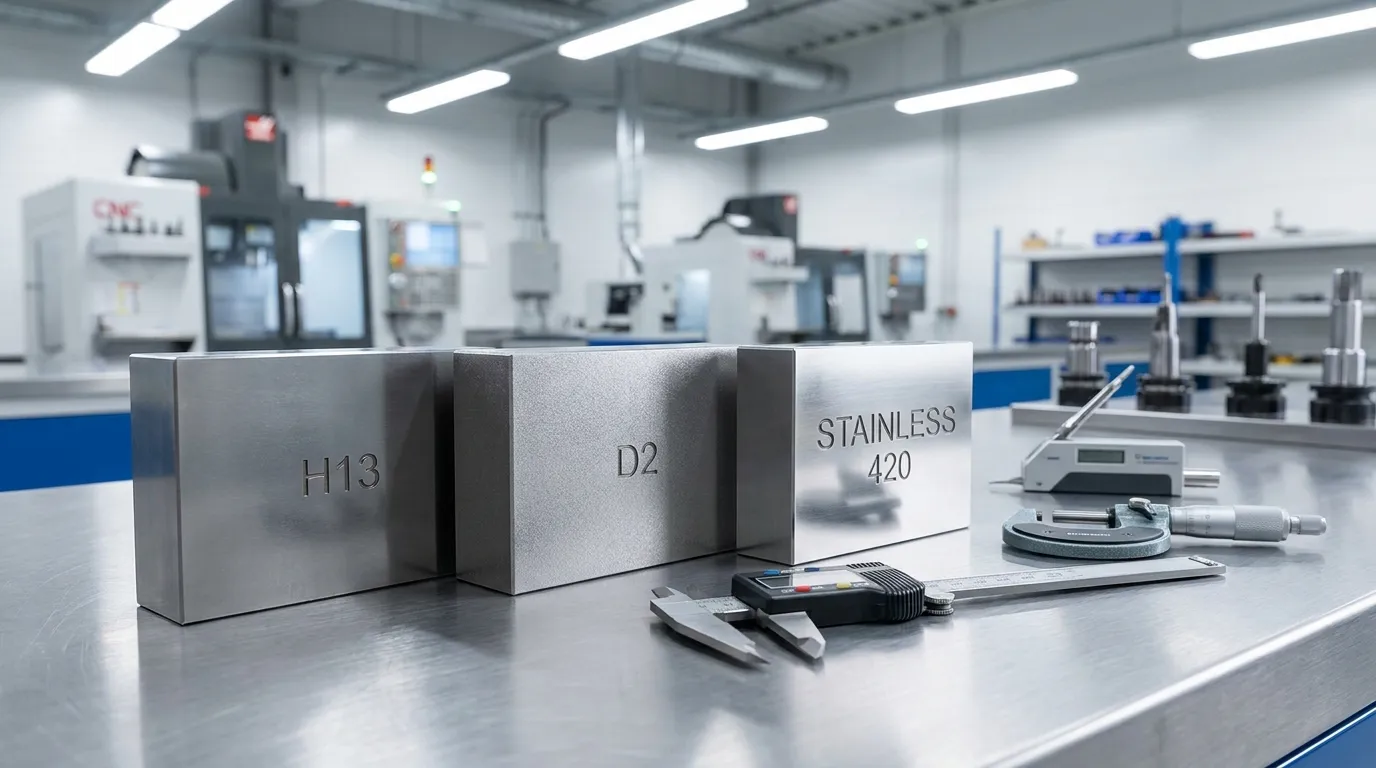
High-wear molding applications often use hardened tool steels like H13, D2, and powder metallurgy grades. The best choice depends on resin abrasiveness, corrosion exposure, polish requirements, and expected cycle count.
Tool steel selection affects both mold life and maintenance cost. Different steels perform better under different molding conditions, especially when abrasive or corrosive plastics are involved.
H13 is one of the most common mold steels because it balances hardness, toughness, and machinability. D2 offers higher abrasion resistance but can become brittle in impact-heavy applications. Stainless grades like S136 improve corrosion resistance, though some stainless steels have lower wear performance than hardened tool steels.
Pesquisa de Stainihard notes that many austenitic stainless steels prioritize corrosion resistance over abrasion resistance. That distinction matters in molds running aggressive fillers or high-cycle production.
Escolha do aço para plásticos preenchidos com vidro
Glass-filled materials create extreme abrasive wear near gates and thin flow channels. Standard pre-hardened steels often wear too quickly in these environments. Powder metallurgy steels or nitrided H13 are more common choices for long production runs.
A cosmetic housing mold creates another tradeoff. Extremely hard tooling may improve wear life, but it can also complicate polishing and surface finishing. Nesses casos, balanced hardness and polishability are usually safer than maximum hardness.
| Grau de aço | Pontos fortes | Limitações | Melhor Uso |
|---|---|---|---|
| H13 | Tenacidade e estabilidade térmica | Resistência moderada ao desgaste | Moldes de produção geral |
| D2 | Alta resistência à abrasão | Menor tenacidade | Resinas abrasivas |
| S136 | Resistência à corrosão | Desgaste menor do que alguns aços para ferramentas | Moldes médicos e cosméticos |
| Aços CPM | Excelente desempenho no desgaste | Custo mais alto | Moldagem abrasiva de alto volume |
For readers comparing broader tooling systems, o Fundamentos do molde plástico page explains how mold design choices affect long-term production performance.
How do coatings improve mold wear resistance?
Surface coatings improve mold wear resistance by reducing friction, surface fatigue, and abrasive damage. Coatings work best when matched with the correct substrate hardness and molding application.
Coatings protect the mold surface rather than changing the entire steel structure. They are commonly used in high-cycle molds where sliding friction or abrasive resin flow causes premature wear.
Physical vapor deposition (PVD) coatings create thin, hard surface layers that reduce friction and improve abrasion resistance. Carbono semelhante a diamante (DLC) coatings are often used on sliding components because they reduce galling and sticking. Nitriding improves surface hardness by diffusing nitrogen into the steel surface.
De acordo com orientações de teste de desgaste publicadas por TWI Global, pin-on-disc testing is commonly used to evaluate coating wear performance under friction conditions.
Quando os revestimentos falham prematuramente
Coatings are not a substitute for poor steel selection. A premium coating applied to weak substrate material often fails faster than properly hardened tool steel without coating. Surface preparation and heat treatment quality still matter.
A high-volume automotive mold may use coated slides to reduce galling and maintenance downtime. If the base steel lacks sufficient hardness, the coating can crack or delaminate under repeated pressure.
| Tipo de revestimento | Principal benefício | Aplicações Comuns |
|---|---|---|
| Revestimento PVD | Redução da abrasão | Portões, cores |
| Revestimento DLC | Menor atrito | Slides, ejectors |
| Nitruração | Endurecimento superficial | Ferramentas gerais de molde |
| Cromagem | Proteção contra corrosão | Superfícies selecionadas da cavidade |
Moldes que exigem acabamentos cosméticos frequentemente combinam revestimentos com especializações Opções de acabamento superficial to maintain appearance quality and reduce polishing frequency.
Which heat treatments improve wear resistance in mold tooling?
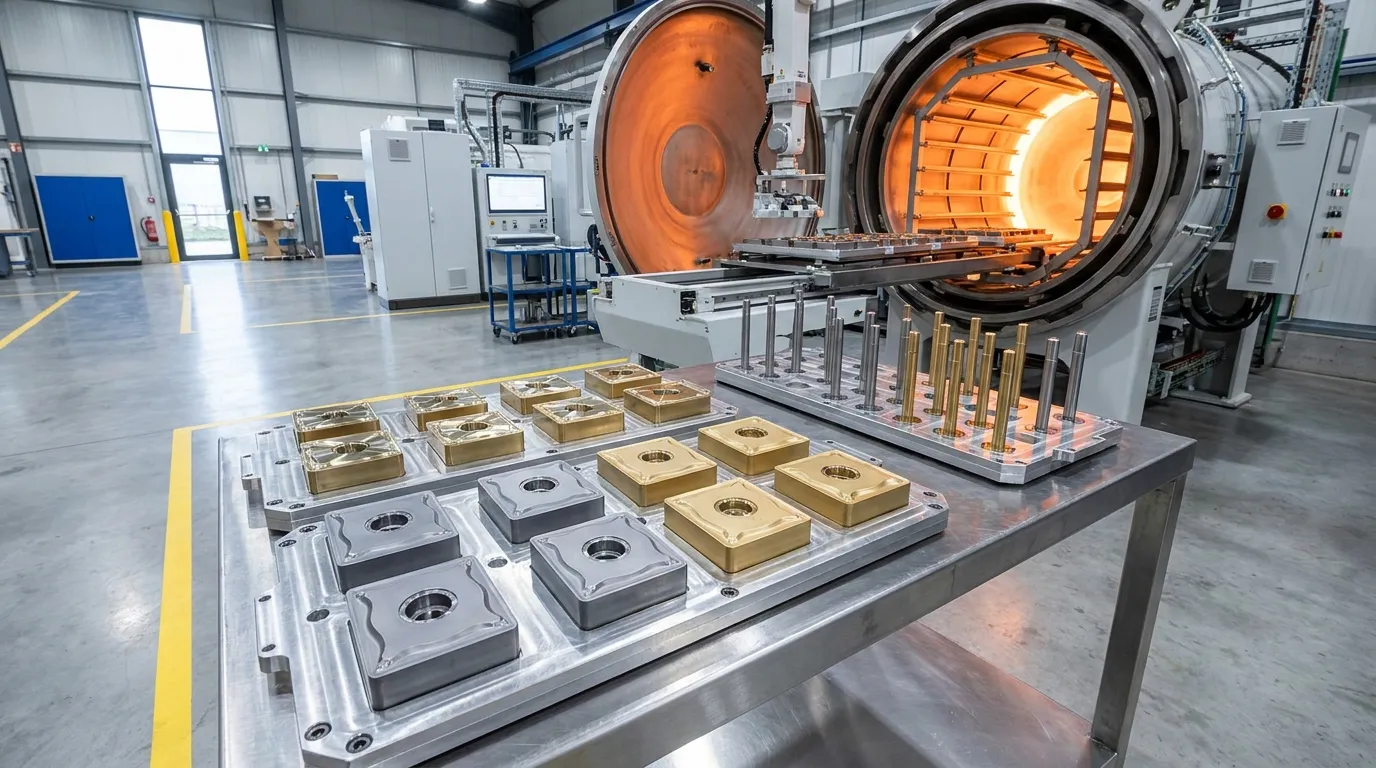
Heat treatment improves mold wear resistance by increasing surface hardness and stabilizing the steel structure. The wrong process can also increase brittleness, distortion, or cracking risk.
Heat treatment changes the internal structure of the steel. In mold manufacturing, this process affects hardness, toughness, Estabilidade dimensional, e durabilidade a longo prazo.
Vacuum hardening is commonly used because it limits oxidation and supports consistent hardness throughout the mold component. Tempering follows hardening and helps reduce brittleness by relieving internal stress. Case hardening and nitriding improve surface hardness without fully hardening the entire part.
Por que a nitruração é comum em moldes de injeção
Nitriding creates a hard outer layer while maintaining a tougher core underneath. That balance works well for slides, ejector systems, and components exposed to repeated friction. It also reduces distortion risk compared to some deeper hardening processes.
A mold running mineral-filled flame-retardant resin may experience rapid ejector pin wear. Em muitos casos, nitrided ejector systems extend maintenance intervals and reduce galling problems.
| Tratamento térmico | Principal benefício | Risco Comum |
|---|---|---|
| Endurecimento a vácuo | Dureza uniforme | Distorção se não controlada |
| Têmpera | Alívio do estresse | Dureza reduzida se excessiva |
| Nitruração | Resistência ao desgaste superficial | Profundidade limitada |
| Cementação | Exterior rígido | Complexidade do processo |
Uma explicação detalhada de Processo de tratamento térmico methods can help engineers match steel grades with suitable hardening strategies.
How do abrasive plastics reduce mold life?
Abrasive engineering plastics can rapidly damage mold surfaces, especially around gates and high-flow regions. Glass-filled resins often require upgraded steel grades, coatings, or nitrided surfaces.
Filled plastics behave differently from standard commodity resins. Glass fibers, flame retardants, and mineral additives increase friction against the mold surface during every injection cycle. High-flow regions typically show wear first.
Glass-filled nylon is one of the most common causes of premature mold wear. Gates lose dimensional accuracy, core surfaces become rougher, and flash begins appearing earlier in production runs.
| Tipo de resina | Risco de desgaste | Recomendação típica |
|---|---|---|
| PP padrão | Baixo | Aço pré-temperado |
| Náilon preenchido com vidro | Alto | Aço endurecido ou nitrutrado |
| Compostos retardantes de chama | Médio a alto | Ferramentas revestidas |
| Resina preenchida com minerais | Alto | Inserts resistentes ao desgaste |
A low-volume prototype mold may avoid expensive coatings because production volume does not justify premium treatment costs. High-volume production molds usually benefit from stronger wear protection because maintenance downtime becomes far more expensive over time.
Processing temperatures, injection pressure, and resin flow speed also influence wear behavior. Following proper Diretrizes de moldagem can help reduce unnecessary tooling stress.
How do you choose the right wear-resistance strategy?
The best wear-resistance strategy balances tooling cost, Volume de produção, resin abrasiveness, and maintenance downtime. Overengineering the mold can waste budget, while underengineering increases repair frequency.
There is no single material or coating that works for every mold. The correct choice depends on resin type, expected cycle count, Requisitos cosméticos, and budget limitations.
High-volume automotive tooling usually justifies premium steels and coatings because downtime costs are high. Prototype molds and short production runs often use lower-cost tooling strategies instead.
Tabela de Decisão de Desgaste por Mofo
| Cenário de Produção | Aço Recomendado | Revestimento ou Tratamento | Risco de Manutenção |
|---|---|---|---|
| Protótipo de baixo volume | Aço pré-temperado | Tratamento mínimo | Moderado |
| Mofo cosmético da carcaça | S136 | Nitruramento leve | De baixo a moderado |
| Molde de náilon preenchido com vidro | H13 ou aço CPM | Nitruração ou DVP | Baixo |
| Molde automotivo de alta velocidade | Aço D2 ou CPM | DLC ou PVD | Muito baixo |
| Molde de resina preenchido com minerais | Aço para ferramentas endurecido | Nitruração | Moderado a baixo |
A mold producing abrasive parts around the clock may recover coating costs quickly through reduced maintenance. On the other hand, a short-run mold may never recover that added expense.
Leitores que avaliam o ROI das ferramentas podem comparar de forma mais ampla Análise de custos de ferramentas factors when deciding how much wear protection makes financial sense.
What maintenance signs indicate poor wear resistance?
Poor wear resistance usually appears gradually before major tooling failure occurs. Early warning signs include flash, dimensional drift, polishing frequency increases, and rough surface finishes.
Slides and ejector systems may begin sticking or galling. Gates can lose edge definition, especially in molds processing abrasive fillers. Surface scratches and drag marks often appear before more serious dimensional issues develop.
Lista de Verificação de Solução de Problemas de Falha de Desgaste
| Sintoma | Causa provável | Solução recomendada | Urgência |
|---|---|---|---|
| Clarão no desligamento | Desgaste superficial | Retrabalho ou inserção mais dura | Alto |
| Avaria em slides | Falha de lubrificação ou revestimento ruim | Revestimento ou nitruração | Médio |
| Polimento frequente | Desgaste por resina abrasiva | Atualizar aço ou revestimento | Médio |
| Acabamento da cavidade rugosa | Fadiga superficial | Revisão do tratamento superficial | Médio |
| Pino ejetor travando | Desgaste adesivo | Tratamento de superfícies mais duras | Alto |
Preventive maintenance matters as much as material selection. Even premium tooling can wear prematurely if lubrication, cooling, or processing conditions are poorly controlled.
Acertando o Próximo Passo
Choosing the right wear resistance strategy starts with understanding the molding environment. Resin abrasiveness, Volume de produção, Requisitos de acabamento superficial, and maintenance expectations all affect tooling decisions.
Many mold failures come from mismatched material choices rather than poor manufacturing. Harder steel is not always better, and coatings are not magic fixes for weak substrates. The most reliable molds use balanced engineering decisions across steel selection, Tratamento térmico, and surface protection.
If your mold is already showing gate wear, Galling, or dimensional drift, reviewing the tooling material and treatment process is usually the best place to start.
Perguntas Frequentes
What is wear resistance in mold components?
Wear resistance is the ability of a mold component to resist material loss caused by friction, abrasion, and repeated molding cycles. Better wear resistance helps molds maintain dimensional accuracy and surface quality during longer production runs.
Does higher hardness always improve wear resistance?
Não. Higher hardness can improve abrasion resistance, but excessive hardness may reduce toughness and increase cracking risk. Mold performance depends on balancing hardness, toughness, coatings, e condições de operação.
Which mold steel is best for glass-filled plastics?
Hardened tool steels such as H13, D2, and some powder metallurgy grades are commonly used for abrasive glass-filled materials. The best option depends on corrosion exposure, polish requirements, and expected production volume.
How do coatings improve mold life?
Coatings reduce friction, surface fatigue, and abrasive wear on mold surfaces. Properly matched coatings can extend maintenance intervals and reduce premature wear in high-cycle molding applications.
What causes rapid wear in injection molds?
Resinas abrasivas, Lubrificação ruim, sliding friction, and high production cycles are common causes of rapid mold wear. Glass fibers and mineral fillers are especially damaging to gates, cores, and sliding surfaces.
Is nitriding good for mold components?
Sim. Nitriding improves surface hardness and wear resistance while maintaining core toughness. It is commonly used for slides, ejector systems, and tooling exposed to repetitive friction.
Compartilhar:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
