



Injection Molding Mold Parts: Núcleo, Cavidade, Ejeção, and Guide Parts
Injection molding mold parts include the core, cavity, Sistema ejetor, Componentes do guia, runners, gates, Canais de resfriamento, and venting features. These systems work together to shape plastic parts, maintain alignment, control resin flow, and release finished products safely. High-quality mold components improve dimensional accuracy, reduce wear, prevent defects like flashing or sticking, and help manufacturers maintain stable production across long production runs.
Injection molds work as complete systems, but every system depends on the quality of its individual parts. A worn guide bushing, poorly positioned ejector pin, or inefficient cooling channel can create defects even when the rest of the mold looks fine. Understanding how these components work together helps engineers, buyers, and production teams make better tooling decisions and avoid expensive downtime later.
What are the main parts of an injection molding mold?
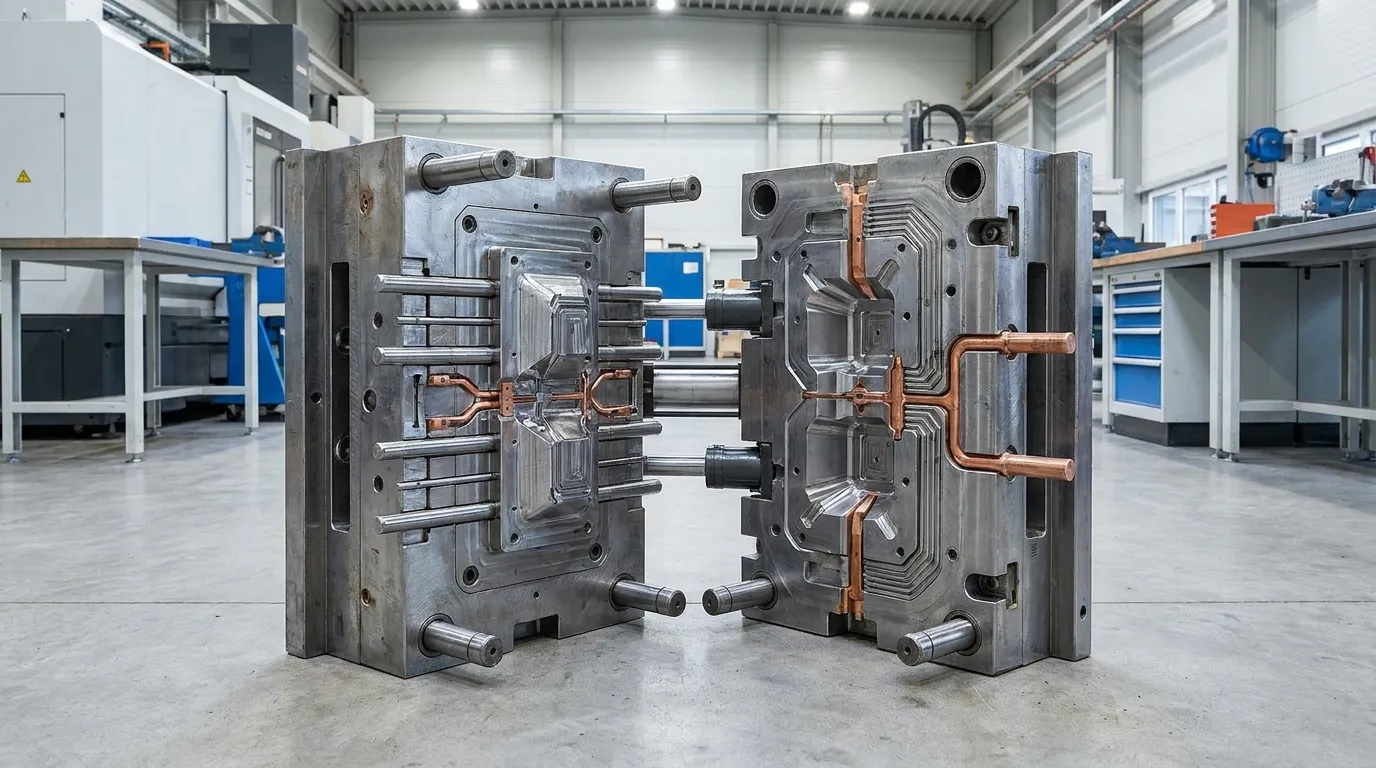
Injection molding mold parts are usually grouped into forming, Alinhamento, Ejeção, Resfriamento, and flow-control systems. Each group affects part quality, mold life, and production consistency in different ways.
Most injection molds contain the same core component groups, even when part designs vary. The core and cavity create the molded shape, alignment parts keep mold halves positioned correctly, and ejection systems remove cooled parts after molding. Canais de resfriamento, runners, and gates manage heat and resin flow throughout the cycle.
If you need a broader breakdown of complete mold architecture, isso Visão geral dos componentes do molde explains how these systems connect inside a full tooling setup.
De acordo com o Visão geral da moldagem por injeção na Wikipédia, standard molds also include venting features, mold plates, and clamping systems that support pressure and alignment during production.
Tabela de Funções dos Componentes do Molde de Injeção
| Grupo Componente | Função principal | Risco de Falha Comum | Impacto na Produção |
|---|---|---|---|
| Núcleo e cavidade | Geometria da peça de forma | Desgaste e desajuste | Flashing, dimensional errors |
| Sistema de guias | Manter o alinhamento | Desgaste das buchas | Defeitos na linha de separação |
| Sistema de ejeção | Remoção das peças moldadas | Dano nos pinos | Scratches, Fixação |
| Sistema de corredores e portões | Fluxo direto de resina | Desgaste do portão | Planos curtos, imbalance |
| Sistema de resfriamento | Controle a temperatura do molde | Fluxo de resfriamento ruim | Deformação, long cycle times |
| Sistema de ventilação | Libere ar aprisionado | Ventilações bloqueadas | Marcas de queimadura, incomplete filling |
What is the difference between the core and cavity?
The cavity forms the external shape of the plastic part, while the core creates internal features and hollow sections. Both must stay precisely aligned to avoid flash, Deformação, or dimensional defects.
The cavity side usually creates the visible outside surface of the molded part. The core side forms internal details such as holes, costelas, or mounting structures. During injection, molten resin fills the space between these two surfaces to create the finished component.
Um detalhado Fundamentos do molde de injeção guide can help if you want to understand how the full molding cycle supports these forming surfaces.
| Característica | Núcleo | Cavidade |
|---|---|---|
| Papel principal | Cria geometria interna | Cria a forma externa |
| Exposição | Alta pressão e atrito | Altas exigências de acabamento superficial |
| Problema comum de desgaste | Abrasão e aderência | Riscos superficiais |
| Impacto na qualidade | Dimensões internas | Aparência cosmética |
The core often experiences higher mechanical stress because parts shrink around it during cooling. This is why ejector placement matters so much. If the core surface grips the plastic too tightly, the ejection system can damage the finished part during release.
Por exemplo, medical device housings often require highly polished cavity surfaces to maintain cosmetic quality. At the same time, the core may need hardened steel inserts to resist wear from repeated production cycles.
Which mold parts control alignment and precision?
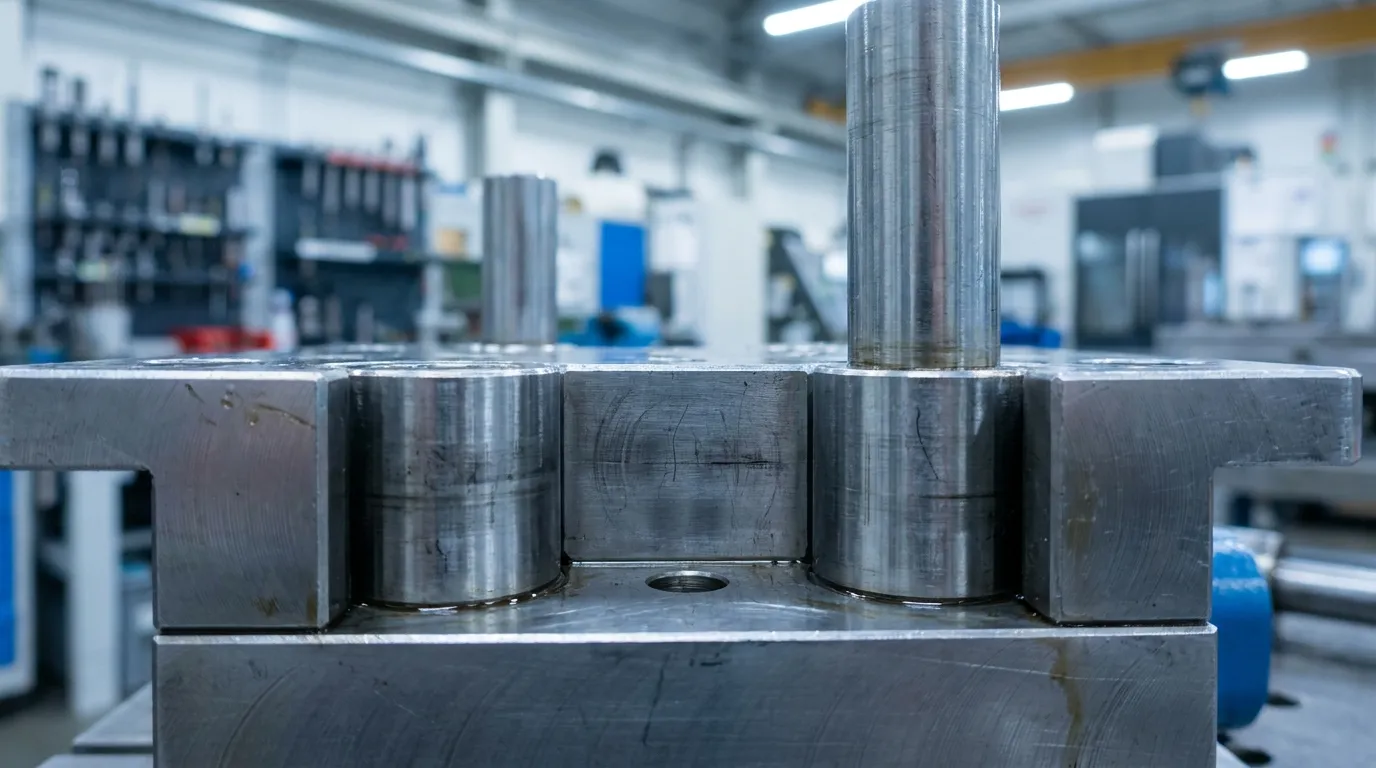
Guide posts and bushings keep mold halves aligned during every cycle. Poor alignment increases wear, flashing, part mismatch, and long-term tooling instability.
Alignment systems control how accurately the mold closes during production. Even slight misalignment can create flashing at the parting line or uneven pressure across the cavity surface. Com o tempo, this accelerates mold wear and reduces dimensional consistency.
O Componentes do guia section explains how precision alignment parts support repeatable molding performance.
De acordo com o Guia de componentes de moldes Agilian, guide pins and bushings are among the most important wear surfaces inside production tooling.
Tabela de Falhamento de Alinhamento Se-Então
| Se isso acontecer | Causa Provável | Resultado da Produção |
|---|---|---|
| Flashing na linha de separação | Buchas guia gastas | Vazamento excessivo de resina |
| Pressão desigual na cavidade | Metades do molde desalinhadas | Distorção de peças |
| Desgaste rápido nas bordas das cavidades | Baixa repetibilidade do alinhamento | Vida útil reduzida do molde |
| Descompasso de superfície | Postes de guia danificados | Defeitos visíveis nas peças |
Lower-cost guide systems are not always the best long-term option. They may work for short production runs, but high-cycle molds usually need hardened alignment components to maintain precision over time.
An automotive interior trim mold is a good example. After extended production cycles, worn guide bushings often create flashing along visible edges. Replacing only the cavity inserts rarely fixes the issue if alignment wear caused the original problem.
How does the ejection system remove molded parts?
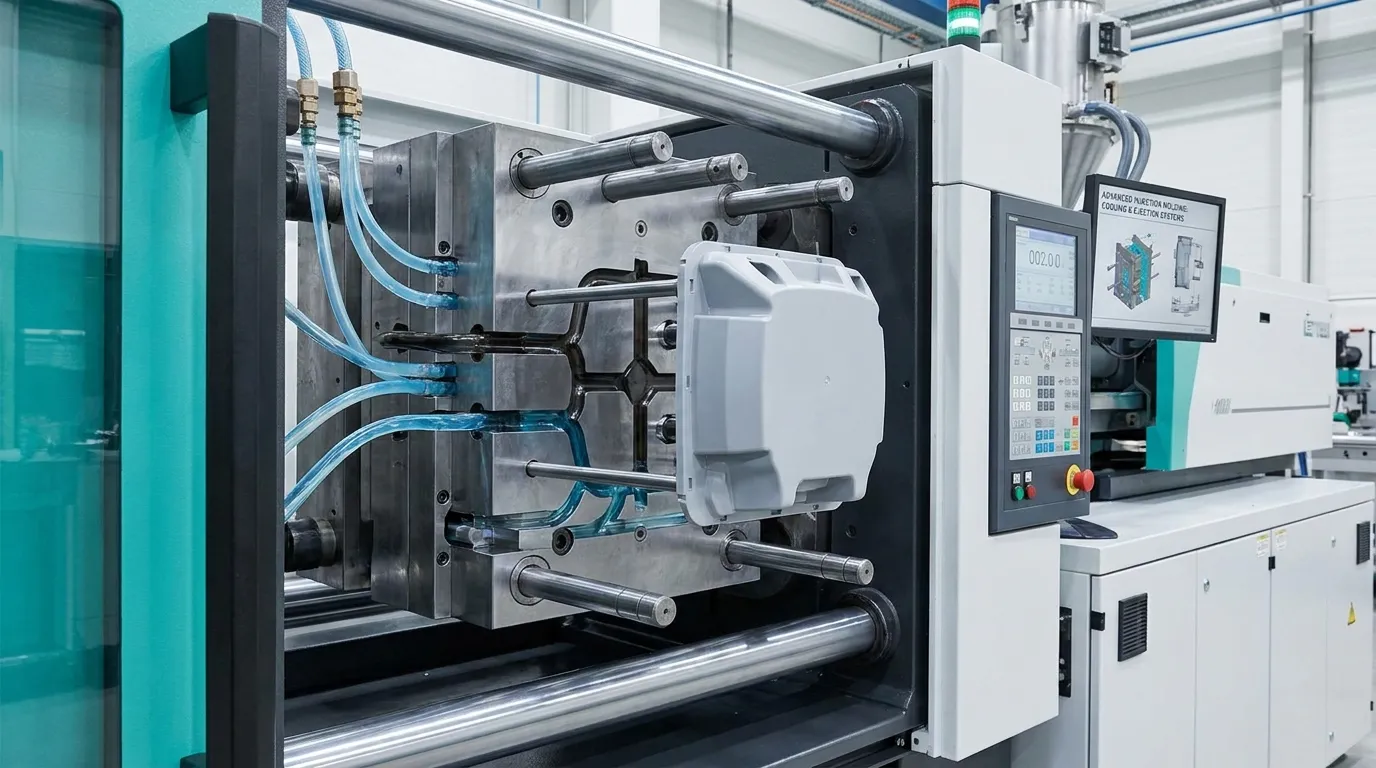
Ejection systems push cooled plastic parts out of the mold after solidification. Incorrect ejector placement can leave marks, crack parts, or create deformation during release.
Após o resfriamento, the mold opens and the ejection system pushes the finished part away from the core. Most molds use ejector pins, ejector sleeves, or stripper plates depending on part geometry and surface requirements.
O Peças do sistema ejetor guide provides additional detail about common ejection hardware used in production molds.
A standard ejection sequence usually follows these steps:
- The mold opens after cooling.
- Ejector plates move forward.
- Ejector pins contact the molded part.
- The part separates from the core.
- The ejector system retracts before the next cycle.
Different parts require different ejection strategies. Thin-wall parts often need carefully distributed ejector pins to avoid deformation. Cosmetic housings may use sleeves or stripper systems to reduce visible marks.
Problemas comuns de ejeção
| Problema | Causa Provável | Resultado |
|---|---|---|
| Marcas de alfinete | Pressão excessiva do ejetor | Defeitos cosméticos |
| Fixação de peças | Ângulo de tiragem ruim | Ciclo de interrupção |
| Rachaduras | Força de ejeção desigual | Peças de sucata |
| Deformação | Temporização da ejeção a quente | Instabilidade dimensional |
Replacing worn ejector pins without inspecting alignment components can waste time and money. Ejection problems sometimes start with mold misalignment, not the pins themselves.
A medical electronics housing illustrates this well. Poor ejector placement near cosmetic surfaces can leave visible witness marks, even when molding conditions stay within normal production ranges.
What do runners, gates, and cooling channels do?
Runners and gates direct molten plastic into the mold cavity, while cooling channels remove heat for stable cycle times. Poor flow or cooling design often causes short shots, Deformação, or sink marks.
The runner system moves molten resin from the injection unit into the cavity. Gates control how resin enters the part itself. Cooling channels then remove heat so the molded component solidifies evenly before ejection.
De acordo com o Entrada da Wikipédia sobre moldagem por injeção, cooling systems strongly influence cycle time and dimensional consistency during production.
| Sistema | Cargo Principal | Questão comum |
|---|---|---|
| Corredor | Move resina através do molde | Desequilíbrio de fluxo |
| Portão | Controla a entrada da cavidade | Congelamento do portão |
| Canal de resfriamento | Remove calor | Resfriamento desigual |
| Vento | Libera ar aprisionado | Marcas de queimadura |
Cooling design becomes especially important in high-cavitation molds. A consumer electronics mold producing multiple thin-wall housings may require upgraded cooling channels to maintain stable cycle times across every cavity.
Por que a ventilação importa em moldes de injeção
Vents allow trapped air to escape as molten resin fills the cavity. Without proper venting, compressed air can create burn marks, Chutes curtos, ou preenchimento incompleto.
O Guia de solução de problemas do Elastron notes that poor venting often contributes to filling defects and trapped gas problems during molding cycles.
Complex custom runner systems are not always necessary. Standardized runner layouts often simplify maintenance and reduce downtime for many production programs, especially when part geometry remains relatively simple.
Which injection mold parts wear out the fastest?
Pinos ejetores, gates, Buchas, and high-friction inserts usually wear out first because they experience constant movement, Pressão, and heat exposure during molding cycles.
Moving and high-contact components naturally wear faster than static mold plates. Volume de produção, Abrasividade da resina, and maintenance practices all affect how quickly this happens.
O Componentes de desgaste do molde section helps production teams identify common replacement areas before failures disrupt production.
Lista de Verificação de Componentes de Mofagem de Alta Durabilidade
| Componente | Por que ele se desgasta | Sintoma comum |
|---|---|---|
| Pinos ejetores | Movimento constante de deslizamento | Marcas de alfinetes ou de alfinetes |
| Buchas guia | Contato repetido de alinhamento | Flashing |
| Portões | Alta velocidade da resina | Inconsistência de preenchimento |
| Inserts | Atrito e calor | Deriva dimensional |
O Perguntas Frequentes sobre moldagem por injeção ESCATEC explains that mold lifespan depends heavily on steel quality and operating conditions.
A buyer choosing between hardened steel ejector pins and untreated components should consider production volume carefully. Lower-cost untreated pins may work for short runs, but hardened components usually last much longer in continuous manufacturing environments.
Interchangeable inserts also wear differently depending on resin type. Glass-filled materials often accelerate abrasion on cavity inserts compared to standard resins.
What should buyers check before sourcing mold components?
Buyers should verify tolerance capability, Grau de aço, Qualidade do tratamento térmico, Acabamento superficial, and supplier delivery performance before ordering mold components for production tooling.
Mold components directly affect production reliability, so sourcing decisions should focus on consistency instead of price alone. Poorly machined or untreated components can create repeat maintenance issues that cost far more than the original savings.
Fabricantes procurando Componentes padrão de molde should compare material specifications, machining precision, and lead-time stability before placing production orders.
Lista de Verificação para Compradores de Componentes de Mofo
- Confirme as especificações de grau e dureza do aço
- Verificar a capacidade de tolerância para peças de precisão
- Revise a documentação do processo de tratamento térmico
- Verifique os requisitos de acabamento superficial
- Compare os prazos de entrega da substituição
- Determine se as peças são padrão ou personalizadas
- Avalie a consistência dos fornecedores em pedidos repetidos
Custom mold components are not always necessary. Standardized parts often simplify future maintenance because replacements remain easier to source and install.
Por exemplo, a consumer electronics supplier using interchangeable cavity inserts can support multiple product versions without building entirely new molds. This lowers tooling costs and shortens revision lead times during product updates.
How do mold component failures affect production quality?
Mold component failures directly affect dimensional consistency, Qualidade da superfície, e estabilidade de produção. Many common molding defects trace back to worn or poorly maintained tooling parts instead of machine settings alone.
O Peças de molde de precisão resource explains how tooling accuracy supports repeatable molding performance across long production runs.
Matriz de Solução de Problemas de Defeitos de Mofo
| Defeito | Provável Componente Falhado | Causa Comum | Inspeção Recomendada |
|---|---|---|---|
| Flashing | Buchas guia | Desalinhamento do mofo | Verifique o desgaste do alinhamento |
| Cena curta | Portão ou ventilação | Fluxo restrito | Inspecionar a condição do portão |
| Marcas de queimadura | Sistema de ventilação | Gás aprisionado | Limpar canais de ventilação |
| Fixação | Sistema de ejeção | Força de liberação ruim | Inspecionar o movimento do ejetor |
| Deformação | Canais de resfriamento | Temperatura irregular | Verifique o fluxo de resfriamento |
Many processors adjust injection pressure first when flashing appears. That approach does not always solve the root issue. If guide systems are worn, the mold may continue leaking resin even with lower processing pressure.
Cooling problems create similar confusion. Uneven cooling channels often cause warping that operators mistakenly blame on material shrinkage or cycle timing. Inspecting the cooling layout usually reveals the real problem faster.
O que fazer a seguir
Understanding injection molding mold parts helps manufacturers make better tooling decisions before problems appear on the production floor. The core, cavity, guide system, Canais de resfriamento, and ejector components all affect mold life and part quality in different ways.
If you're evaluating tooling suppliers or replacing worn mold components, focus on precision, material quality, and long-term repeatability instead of upfront cost alone. Standardized components can simplify maintenance, but high-cycle molds may still require upgraded materials and tighter tolerances for stable production over time.
Perguntas Frequentes
What are the components of an injection mold?
Injection molds contain several functional component groups. These usually include the core, cavity, Sistema ejetor, Pinos guia, Buchas, runners, gates, Canais de resfriamento, and venting features that support molding, Alinhamento, and part release.
What is the core and cavity in injection molding?
The cavity and core are the primary forming components inside the mold. The cavity creates the outside shape of the part, while the core forms internal geometry and hollow sections during molding.
What do ejector pins do in injection molding?
Ejector pins safely remove molded parts from the cavity after cooling. Proper pin placement helps prevent sticking, rachaduras, and visible surface marks during the ejection stage.
Which mold components wear out fastest?
High-friction and moving components usually wear out first. Pinos ejetores, Buchas guia, Inserts, and gates experience repeated heat, Pressão, and motion during production cycles.
What causes flashing in injection molds?
Flashing happens when molten plastic escapes between mold surfaces. Worn alignment components, damaged guide bushings, or poor mold closure often allow resin leakage at the parting line.
How long do injection mold components last?
Mold component lifespan depends on steel quality, resin type, maintenance practices, and production volume. Hardened steel components generally last longer in high-cycle manufacturing environments.
Compartilhar:



Escrito por Sunshine
Em Sol, Somos um fabricante e fornecedor profissional de componentes de moldes de precisão, oferecendo uma ampla variedade de produtos para aplicações de estampagem e molde por injeção. Nosso foco principal inclui a formação de matrizes, pinos e mangas ejetor, e postes guia e buchas. Com usinagem CNC avançada, Controle rigoroso de qualidade, e fortes capacidades de produção, Garantimos confiabilidade, Peças de alta precisão, juntamente com componentes padrão em estoque para fornecimento global rápido e eficiente.
NOTÍCIAS
RECEBA O SERVIÇO
Com peças de qualidade para todos os orçamentos e equipe amigável treinada para tornar sua visita informativa e sem complicações.
